How to Record Feeder Breaker Scraper Width for Replacement Sourcing
Record feeder breaker scraper width with defined endpoints, intact-flight checks, repeat measurements, photos, and clear separation from nominal drawings.
Engineering GuideUpdated سبتمبر 16, 2026
Scraper width is one of the dimensions that can quickly separate feeder breaker chain configurations, but it is also vulnerable to field ambiguity. A flight may have worn ends, built-up material, bent corners, replaced scraper plates, weld repairs, or attachments that make the “outside width” look different depending on where the tape is placed. Recording the number without defining the endpoints can therefore create a false match.
On the documented feeder breaker products used by this site, width is an important discriminator. K201B is listed with a scraper width of 44 2/5 inches (1127.5 mm), while K207B is listed at 46 inches (1171.85 mm). Both are nominal 3 1/2 inch pitch chains. That difference is exactly why width should be measured and documented carefully rather than inferred from pitch or from the overall machine width.
This guide focuses on replacement sourcing. It does not establish a wear limit for scraper bars or prescribe how a machine must be opened for access. Use the feeder breaker manufacturer’s procedure and site isolation rules before entering the chain area, and treat any damaged or uncertain geometry as evidence that needs review rather than something to straighten or modify for the sake of a measurement.
Define the endpoints
State whether the width runs between outer scraper edges, controlled faces, or another drawing-defined feature.
Use an intact reference
Prefer a representative undamaged flight and repeat the measurement on additional flights when possible.
Preserve the deviation
If the field value differs from the old drawing, record both values and investigate instead of rounding the chain back to the expected model.
1. Confirm What “Scraper Width” Means for the Assembly in Front of You
Before measuring, identify the conveying element that will define the width. Some records may call it a scraper, flight, flight bar, scraper head assembly, or a combination of a head and plate. The name is less important than making sure the same physical faces are used in the field and on the comparison drawing. If the old drawing gives a dimension to a controlled face that is not the extreme worn edge, reproduce that reference in the field instead of measuring the easiest outside-to-outside distance.
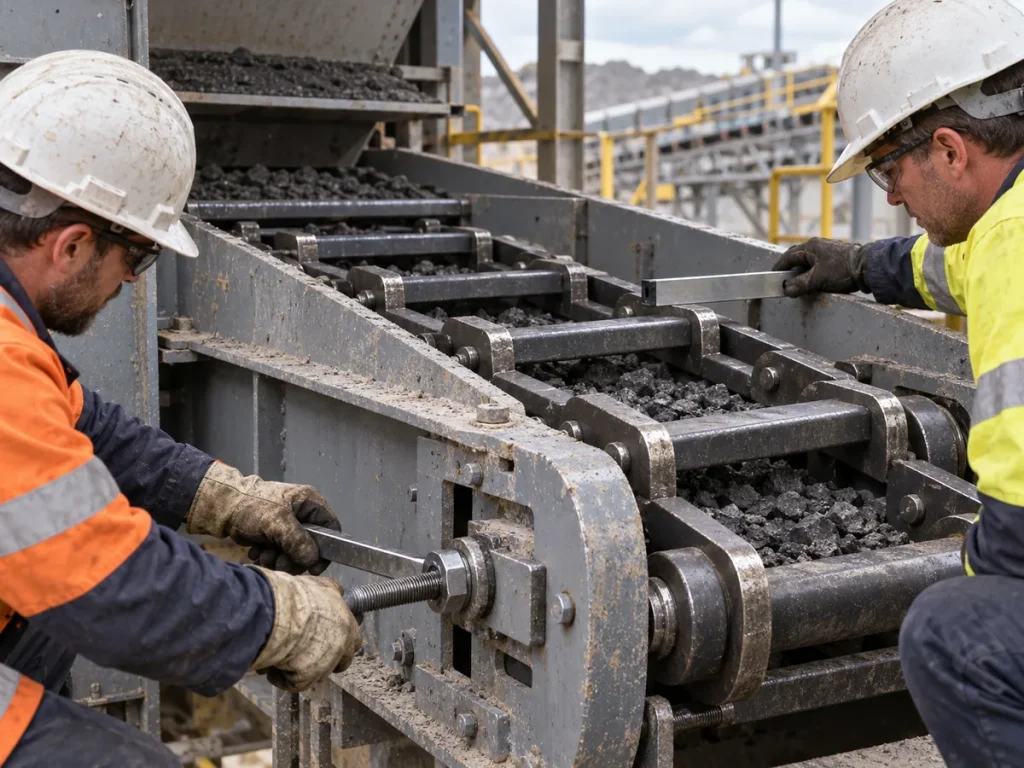
Photograph the complete flight and mark the proposed endpoints on a copy of the image or inspection sheet. This simple step catches many misunderstandings before a number is entered into the RFQ. If the chain has multiple flight styles or alternating attachments, label which style was measured and whether the pattern repeats consistently around the chain.
2. Select a Flight That Represents the Original Geometry as Closely as Possible
A badly bent or heavily worn scraper can be the reason a replacement is being planned, but it is rarely the best master for sourcing dimensions. Search the accessible chain for an intact flight with no obvious end loss, distortion, weld build-up, or field modification. If no intact flight exists, record several damaged flights and use the drawing or a controlled spare as a second source of evidence.
Do not silently reconstruct a missing corner by eye. If one side of a flight is worn back, record the visible condition and treat the original width as unknown until a drawing, spare, or equivalent intact flight supports it. A measured replacement record is stronger when it openly distinguishes “observed remaining width” from “nominal design width.”
3. Position the Measuring Tool Across the Chosen Reference Faces
Place the tape, steel rule, or suitable measuring tool so it crosses the flight on the intended width line and contacts the two defined reference faces. Avoid an angled measurement from a near corner to a far corner, which produces a longer diagonal value. Where the flight surface is irregular, use a straightedge or other approved aid to project the two reference faces into a plane that can be measured consistently.
Take the reading at a location where the scraper geometry is representative. If the flight is tapered or profiled, state where along its height or depth the measurement was taken. A width recorded at the top edge may not equal a dimension defined at a mounting face. The photograph should show the tool position clearly enough that a reviewer can see which geometry the number represents.
4. Repeat the Measurement and Look for Pattern, Not Just Agreement
Measure more than one flight when safe access allows. The purpose is not to calculate an average automatically; it is to see whether the chain presents a stable repeating dimension or whether wear, repairs, or mixed parts are present. Record each flight separately with its location. If four flights cluster closely and one differs significantly, inspect the outlier before averaging it into a value that describes none of them.
Also compare left and right ends for visible asymmetry. Uneven end wear can be evidence of tracking, side contact, material flow, or another system issue. It may also make an outside-width measurement smaller than the original design. The replacement RFQ should preserve that observation and, when relevant, trigger a broader chain-and-machine inspection rather than simply ordering a wider new flight.
Scraper width measurement checks
Check
Record
Risk if omitted
Flight identity
Location and whether the flight is intact, worn, repaired, or bent
A damaged flight may become the accidental master dimension.
Endpoints
Two physical faces or edges used for the width
Different technicians may measure different features.
Tool position
Height/depth on the flight and whether the tool is square
Diagonal or tapered readings can distort the result.
Repeat readings
Individual values from additional flights
Mixed parts or uneven wear can be hidden by one number.
Drawing comparison
Nominal value and revision stored separately
A field value may be overwritten by the expected specification.
Interface photos
How the scraper/flight connects to chain and pins
Correct width alone does not prove installation compatibility.
Record rule
Do not average unlike or damaged flights into a single “nominal” width. Investigate why the readings differ before selecting the replacement configuration.
5. Compare the Field Record with K201B and K207B Without Forcing a Match
The site’s listed model data provide two useful reference points. K201B has a documented scraper width of 44 2/5 inches (1127.5 mm), while K207B is documented at 46 inches (1171.85 mm). Both have a nominal 3 1/2 inch pitch and a 21 inch repeating unit, so width helps distinguish two assemblies that pitch alone does not separate.
Use those figures as model references, not as targets to which the tape reading must be rounded. If the installed chain measures differently, first check the endpoints and the condition of the chosen flight. Then compare the component arrangement and unit length. A close-but-not-equal width can reflect measurement technique, wear, repair history, a custom chain, or a different model; the website evidence alone cannot decide which explanation is correct.
Observed width
The physical field reading taken between stated reference faces on a stated flight.
Nominal width
The design dimension controlled by an approved drawing or listed model specification.
Endpoint definition
The description of the two edges or faces that establish the width dimension.
Interface evidence
Photographs and dimensions showing how the flight/scraper attaches to the chain assembly.
6. Record Width Together with the Flight-to-Chain Interface
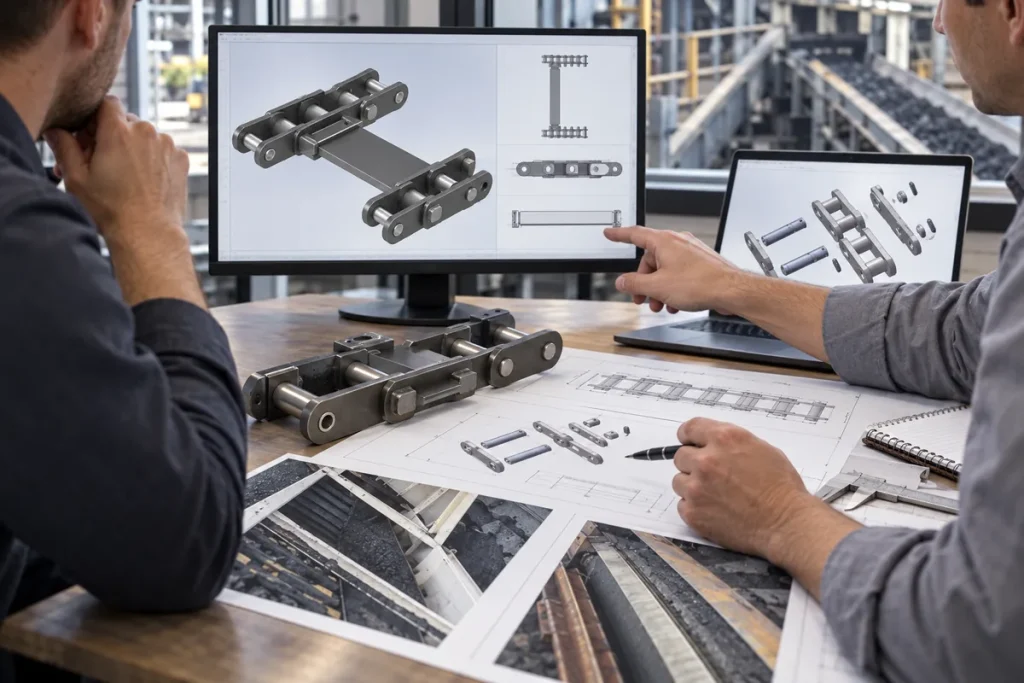
Width tells how far the conveying element spans, but replacement fit also depends on how it connects to the chain. Photograph the scraper head or plate, attachment link, extended pin or retention feature, and the relationship between the two strands. On K207B, for example, the documented component tree includes a Scraper Outer Link and an Extended Pin. On K201B, the documented tertiary components include a Scraper Head and Scraper Plate along with the joint parts.
If a field repair has changed a hole, pin, plate, or fastening detail, record the repair separately. The new chain should not automatically reproduce an undocumented field modification, yet the supplier must know that the installed interface is not identical to the reference drawing. Width plus interface evidence is much more actionable than width alone.
7. Build the RFQ Line Item So the Measurement Cannot Lose Its Meaning
In the RFQ, write the value in a complete statement: “Scraper width measured between [defined faces] on [flight ID/location], field value [number and unit], measured on [date], condition [intact/worn/repaired], photo IDs [references].” If a drawing gives a nominal value, add it in a separate field with the drawing revision. This prevents a purchaser from copying one value into a spreadsheet and losing the reason it was accepted.
When both imperial and metric units are required, identify the original unit of observation and show the conversion separately. Do not round a converted value until the precision needed for the comparison has been agreed. For the listed model data, preserve the documented values as written: K201B 44 2/5 in (1127.5 mm) and K207B 46 in (1171.85 mm).
Use this handoff checklist to close the field record for How to Record Feeder Breaker Scraper Width for Replacement Sourcing. The goal is not to create another generic maintenance form. It is to preserve the specific observations, reference points and machine context that the next reviewer needs in order to understand how the result was obtained. Keep machine-specific acceptance limits under the approved drawing, maintenance procedure or engineering instruction rather than inventing a universal web value.
Checkpoint
ما الذي يجب تسجيله؟
How the record is used
Confirm What “Scraper Width” Means for the Assembly in Front of You
Record the exact machine location, strand or side, current operating/shutdown state, and the observation that relates to confirm what “scraper width” means for the assembly in front of you. Include a photograph that lets another reviewer find the same area.
Establishes the context so later measurements are not detached from the machine and chain position.
Select a Flight That Represents the Original Geometry as Closely as Possible
Capture the physical reference used for select a flight that represents the original geometry as closely as possible. Keep the raw dimension, image or marking beside the interpretation, and note any wear, repair, build-up or access limitation that could affect the reading.
Makes the result repeatable and prevents a damaged or poorly defined reference from becoming the replacement requirement.
Position the Measuring Tool Across the Chosen Reference Faces
Cross-check position the measuring tool across the chosen reference faces against any controlled drawing, previous purchase reference or retained spare that is available. Keep current field data and historical information in separate fields when they differ.
Preserves traceability when field condition, historical records and nominal product information do not agree perfectly.
Repeat the Measurement and Look for Pattern, Not Just Agreement
For repeat the measurement and look for pattern, not just agreement, state what is confirmed, what is only observed, and what still needs engineering confirmation. Attach the image or measurement that supports the statement rather than relying on a product name alone.
Gives maintenance, purchasing and the supplier a clear list of what can be acted on now and what must be resolved before release.
Separate as-found condition from required replacement geometry. A worn, repaired, dirty or partially dismantled component may still be very useful for identification, but its current shape is not automatically the manufacturing requirement. Label field measurements as observed data, retain the original unit and measurement method, and identify any feature that may have been altered by service. For measure feeder breaker scraper width, photographs should show the measurement endpoints or component relationship clearly enough that a remote reviewer can reproduce the logic.
Resolve conflicting information instead of hiding it. If a drawing, old order, marking and current measurement point in different directions, keep each source visible and describe the conflict. Do not average values or silently choose the most convenient one. Use additional photographs, measurements from another intact repeating unit, machine interface information and the controlled document revision to determine which value governs. If build the rfq line item so the measurement cannot lose its meaning cannot be confirmed during the shutdown, state that limitation explicitly so the open question survives the handoff.
Make the next action obvious for How to Record Feeder Breaker Scraper Width for Replacement Sourcing. The completed record should tell maintenance what should be rechecked, tell purchasing what information belongs in the RFQ, and tell engineering which dimensions or interfaces still need approval. Before the machine returns to service, confirm that the file set includes an overall machine view, a complete repeating chain/flight view, close-ups of relevant components or markings, and the dimensions used in this guide. For measure feeder breaker scraper width, a traceable set of observations is more useful than a long narrative with no datum, and it reduces the risk that a replacement decision is made from pitch, appearance or an old part number alone.
Questions to Resolve Before the Next Decision
Should I measure the widest point of the scraper?
Only if the controlled drawing or agreed identification method defines that point as the width reference. If the flight is tapered or has worn corners, identify the exact faces and measurement line used.
What if every flight has a different width?
Keep the individual readings and investigate wear, repair history, mixed components, or measurement-reference differences. Do not average them into a replacement specification until the technical data of the variation is understood.
Can scraper width confirm K201B or K207B?
It is strong supporting evidence but not sufficient alone. Confirm pitch, unit length, component arrangement, flight interface, and application context as well.
Should worn ends be included in the measurement?
Record the remaining observed geometry, but do not assume it represents nominal design width. Pair the field condition with an intact reference, drawing, or engineering review.
Next Step: Close the Measurement Record
For replacement sourcing, scraper width should be a traceable measurement, not a floating number in an email. Define the flight, define the two endpoints, show the measuring tool, repeat the check on other flights, and preserve any difference from the approved drawing.
Then combine width with pitch, repeating unit length, flight spacing, and interface details. That evidence is strong enough to separate plausible feeder breaker configurations and transparent enough to show when the chain still requires engineering identification.