Product Description
ISO16949: 2009 Approved Industrial Chain
Why Choose Us?
1. HangZhou Xihu (West Lake) Dis.hua Chain Group Co., Ltd established in 1991, we have 5 subsidiaries in china and have 6 subsidiaries abroad;
2. we covering a production area of 200,100 square meters, have more than 1,800 sets of advanced equipment and over 3,100 highly skilled employees, the annual production capacity has exceeded 20,000,000meters;
3. we specialized in producing all kinds of standard chains and special chains, such as A or B series chains, driving chains, conveyor chains, hoisting chains, agricultural chains, sprockets, industrial chains, sprockets, gears, wheels and so on;
4. we have obtained ISO9001, ISO14001, ISO16969, AAA and API certificates.
5. Our partners among world top enterprises, such as JOHNDEERE, NEW HOLLAND, CLAAS, HONDA, KUBOTA, YANMAR, etc.
1. Industrial Chain Parts
2. Production flow chart
1. Incoming material
2. Inspection
3. Production of chain board (cold roll steel/punch/heat treatment/shot blasting/cleaning)
4. Production of roller(burr wiping & smear/heat treatment/wiping grinding/cleaning)
5. Production of quill(burr wiping & smear/centerless cylindrical grinding/heat treatment/shining)
6. Production of shaft(cutting/chamfering/heat treatment/ centerless cylindrical grinding/cleaning)
7. Assembling
8. Final inspection
9. Packing
3. Certificate
4. Company Information
HangZhou Xihu (West Lake) Dis.hua Chain Group Co., Ltd was founded in 1 9 9 1, and now it has five wholly owned subsidiaries, one in ZheJiang province, other four in HangZhou, ZHangZhoug province, it is a professional manufacturer of chains, sprockets, tooth gears and various power transmission products.
The group has XIHU (WEST LAKE) DIS.HUA, ZIQIANG brands, is focused on producing all variety of standard roller chains and special chains, such as conveyor chain, stainless steel chain, agricultural chain. With Xihu (West Lake) Dis.hua brand registered in more than 70 countries like America, Europe, Japan, it is building long term cooperation with these world top enterprises, such as JOHNDEERE, NEW HOLLAND, CLAAS, HONDA, KUBOTA, YANMAR.
There is a technical center of province level, Xihu (West Lake) Dis.hua academician working station, experiment station for Xihu (West Lake) Dis.hua post doctors, and national hundreds of program set up in Xihu (West Lake) Dis.hua group. With these platforms and strong technical ability, the more than hundreds of Engineers and technicians have developed all variety of special high precise and high strength products, conducted mold programs for key components in the car and national industry revitalizing program.
Great attention has been paid on environmental protection and energy saving. The product well displays environmental protection and energy saving. In the year of 2 0 0 0, Xihu (West Lake) Dis.hua took the lead in gaining I S O 1 4 0 0 1 environment management certificate and thereafter passed the inspection of clean production and recycling economy, winning the title of “ZHangZhoug Green Enterprise”.
“We are always serving our customers with our best products.”
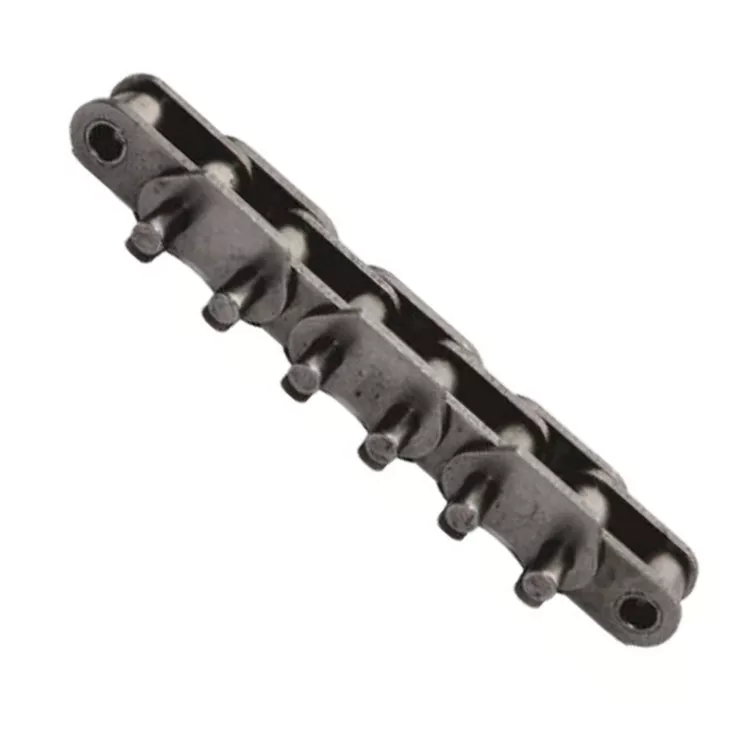
| Usage: | Conveyor Chain |
|---|---|
| Material: | Alloy/Carbon Steel |
| Surface Treatment: | Electroplating |
| Feature: | Heat Resistant |
| Chain Size: | 1/2"*11/128" |
| Structure: | Roller Chain |
| Customization: |
Available
| Customized Request |
|---|
How does a conveyor chain impact energy efficiency in a system?
A conveyor chain plays a significant role in the energy efficiency of a conveyor system. Here are the ways in which it impacts energy efficiency:
1. Reduced Power Consumption:
– A well-designed conveyor chain with low friction characteristics can minimize power consumption. By reducing the frictional resistance between the chain and the conveyor components, less energy is required to move the chain and transport the materials along the conveyor system.
2. Efficient Power Transmission:
– The design and construction of a conveyor chain contribute to efficient power transmission. Chains with optimized pitch, roller diameter, and sprocket tooth profile ensure smooth and effective power transfer, minimizing energy losses during operation.
3. Proper Chain Tensioning:
– Maintaining proper chain tension is crucial for energy efficiency. An adequately tensioned chain ensures optimal contact between the chain and the sprockets, minimizing slippage and power loss. Regular inspections and adjustments of chain tension help maximize energy efficiency.
4. Alignment and Tracking:
– Proper alignment and tracking of the conveyor chain are essential for energy efficiency. Misaligned or poorly tracked chains can cause increased friction, leading to higher energy consumption. Regular monitoring and adjustment of the chain’s alignment ensure smooth and efficient operation.
5. Regular Maintenance:
– Performing routine maintenance on the conveyor chain, including lubrication, cleaning, and inspection, helps maintain optimal performance and energy efficiency. Adequate lubrication reduces friction and wear, minimizing power losses and extending the chain’s lifespan.
6. System Design Optimization:
– Considering energy efficiency during the design phase of a conveyor system can significantly impact its overall efficiency. Proper selection of conveyor chain components, such as low-friction materials and efficient drive systems, can help minimize energy consumption and improve the system’s energy efficiency.
By employing these practices and utilizing energy-efficient conveyor chain technologies, businesses can reduce energy costs, minimize environmental impact, and enhance the overall sustainability of their operations.
How does a conveyor chain handle different types of materials?
A conveyor chain is designed to handle a wide variety of materials in diverse industrial applications. It is capable of efficiently transporting different types of materials, including:
1. Bulk Materials: Conveyor chains are commonly used to handle bulk materials such as grains, coal, ores, aggregates, and powders. The design of the chain, including the spacing and shape of the links, helps prevent material spillage and ensures smooth and consistent flow.
2. Packaged Goods: Conveyor chains are also used for conveying packaged goods such as boxes, cartons, crates, and pallets. They provide a stable and reliable method of transporting these items along the production line, reducing manual handling and increasing productivity.
3. Small Parts: Conveyor chains with specialized attachments or small-pitch configurations are suitable for handling small parts or components. These chains ensure precise positioning and gentle transport of delicate or intricate items.
4. Heavy-Duty Loads: Industrial conveyor chains are capable of handling heavy-duty loads, such as automotive parts, machinery components, and large equipment. They are engineered to withstand the weight and stress of these objects, providing reliable and efficient material handling in demanding environments.
5. Food and Beverage Products: Conveyor chains used in the food and beverage industry are designed to meet strict hygiene and safety standards. They are constructed from materials that are resistant to corrosion, easy to clean, and compliant with food-grade regulations. These chains ensure the safe and contamination-free handling of food products.
6. Hazardous Materials: Conveyor chains can be used to safely transport hazardous materials, such as chemicals or waste products. Specialized chains with additional safety features, such as sealed housings or containment systems, are utilized to minimize the risk of spills or leaks.
Conveyor chains can be customized with different chain configurations, attachments, and accessories to accommodate specific material characteristics and handling requirements. The selection of the appropriate chain type, material, and design parameters ensures optimal performance and efficient material handling for a wide range of materials.
What lubrication is recommended for conveyor chains?
Choosing the right lubrication for conveyor chains is crucial for maintaining their performance and extending their lifespan. Here are some commonly recommended lubricants:
- Chain Oil: Chain oil is specifically designed for lubricating conveyor chains. It provides excellent lubrication, reduces friction, and helps prevent wear and corrosion. Chain oils come in various viscosities to suit different operating conditions.
- Synthetic Lubricants: Synthetic lubricants, such as synthetic oils and greases, offer enhanced performance and durability. They have excellent temperature stability, high resistance to oxidation and degradation, and superior lubricating properties. Synthetic lubricants are suitable for applications with high temperatures, heavy loads, or extreme operating conditions.
- Food-Grade Lubricants: For conveyor chains used in food processing or other industries with strict hygiene requirements, food-grade lubricants are recommended. These lubricants are formulated to be safe for incidental food contact and comply with relevant regulations and standards.
- Dry Film Lubricants: In certain applications where liquid lubricants are not suitable, such as dusty or dirty environments, dry film lubricants can be used. These lubricants form a protective coating on the chain surfaces, reducing friction and preventing wear.
When selecting a lubricant, consider the operating conditions, such as temperature, speed, load, and environmental factors. Consult the manufacturer’s recommendations and guidelines to ensure you choose the appropriate lubrication product for your specific conveyor chain. Regularly monitor the lubrication levels and reapply as needed to maintain optimal chain performance.
editor by CX 2023-08-15