Product Description
| Data(HS-820-K600)Straight Running Plastic Chain | |||||||
| Belt Material | Width W | Working Load | Reverse Radius | Weight | |||
| mm | inch | N(21°C) | lbs(21°C) | mm | inch | kg/m | |
| POM | 152.4 | 6.00 | 1230 | 276 | 50 | 1.97 | 1.25 |
Avantages of the CHINAMFG products
1.CHINAMFG modular conveyor belt has more than 10 times service life,long life time and reducing replacement cost than traditional conveyor belt.
2.CHINAMFG modular conveyor belt is easy to assemble, allowing only the replacement of damaged parts, easy to replace, saving maintenance time and costs.
3.CHINAMFG modular conveyor belt has strong wear resistance, high temperature resistance, cold resistance and oil resistance.
4.CHINAMFG modular conveyor belt is easy to clean, farewell to the propagation of bacteria, especially suitable for application in food industry.
5.CHINAMFG modular conveyor belt in food and non-food industry, it plays an important role in the character of durability,low maintenance cost and easy to clean.
6.CHINAMFG has agents in many countries and can provide good after-sales service.
7.CHINAMFG not only has a complete production line to meet different application needs, but also can provide comprehensive product knowledge and experience. After 20 years of innovative research and development, we can provide more than 5000 kinds of solutions to provide perfect support for you in the field of transportation.
Application
Beverage plant,Beverage filling application,Dairy production plant,Aerosol filling,Glass ware handling
Thermoplastic table top and plate top chains with straight running.
HONGSBELT Plastic chain could install and run on most current chain system and sprocket as well as compatible different industrial standard completely. It makes table top chain be maintained. HONGBELT new chain series has many tip top performances. Such as low friction coefficient, anti-chemical, anti-static, flame-proof and so on.
It could be used for different industries & environment.
Cooperation Case
We Cooperated with DHL & Amazon to Help Them Solve Multi-scenario Application Parcel Sorting
Global cooperation broke through 50+ agent service providers
and signed strategic cooperation agreements with “Safari Belting Systems” in the United States
“HONG’S BELT Branches” in Europe, and “HONG’S BELT Branches” in India
Exhibitions around the world
Every year CHINAMFG will go to all over the world to participate in exhibitions
We have served projects in more than 120 regions and countries with global delivery capabilities
Hong’s Belt team can provide customers with more than 5,000 solutions
Factory
HONG’S BELT
Xihu (West Lake) Dis. Xinhai (HangZhou) Technology Co., Ltd is a leading high-tech company providing intelligent conveyor solutions. We have a modern industrialized manufacturing area of 100,000 square CHINAMFG for the production of modular plastic belts and conveying systems solutions.
Hong’sbelt Group currently has more than 1,000 employees, including more than 100 R&D teams, more than 500 production and functional departments, and about 300 sales and sales support departments. The sales points are distributed on all continents of the world.Realize Automatic and Intelligent.
We developed a fully integrated industrial chain with independent core technology, key components, leading products and conveyor systems solutions.
Certificate
We hold more than 400 national authorized patents and software certifications
Allseries of products have obtained the US “FDA” food grade certification And “EU” certification in Europe
Obtained “ISO9001-2008” quality management system certification
FAQ
Q: Are you a trading company or manufacturer?
A: We are a manufacturer of modular belt, chains belt and conveyor components, with head office in HangZhou, China, and 2 big factories located in HangZhou and HangZhou.
Q: Are HONGSBELT products in accordance with FDA regulations and EU Directives?
A: Our standard materials (PP, POM, PE, PA) comply with the FDA regulations and EU Directives. A letter of assurance can be made available on demand.
Q: Can we use HONGSBELT Modular Conveyor Belt in corrosive environment?
A: HONGSBELT belts can be used in medium to severe CHINAMFG applications, however, special product recommendations and conveyor design guidelines must be followed. More information, pls contact our online Customer Service or email to HONGSBELT Team.
Q: What is the temperature range for the belt material?
A: HONGSBELT belts offers various materials suitable for operation in temperatures ranging from -60 °C to 260 °C. Specific material should be chosen based on your operating temperature.
Q: What is the real meaning of the belt strength?
A: The belt strength is the maximum tension (per foot or meter of width) the belt can continuously run at.
Q: How long will it take me to get quotation?
A: You will always receive any requested quote by the end of the next working day at the latest, but often quotes are emailed to you before you hang up the phone.
| Material: | POM–Dp,POM-Lf |
|---|---|
| Structure: | Top Chain |
| Surface Treatment: | Plastic |
| Chain Size: | 3.048m/Box |
| Feature: | Fire Resistant, Oil Resistant, Heat Resistant |
| Pin Material: | Cold Rolled Austenitic Stainless Steel |
| Samples: |
US$ 17.5/Meter
1 Meter(Min.Order) | |
|---|
What are the benefits of using an overhead conveyor chain system?
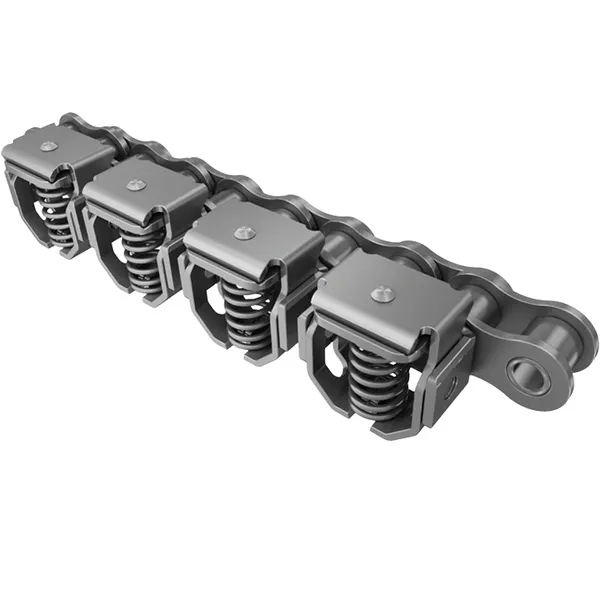
Using an overhead conveyor chain system offers several benefits in various industrial applications. Here are some key advantages:
1. Space Optimization:
– Overhead conveyor chain systems utilize the vertical space, allowing efficient utilization of floor space. This is especially beneficial in facilities with limited floor area, as it enables efficient material handling and production flow without obstructing the work area.
2. Flexibility and Versatility:
– Overhead conveyor chains offer flexibility in routing and can be customized to fit the specific layout requirements of the facility. They can traverse different areas, including assembly lines, paint booths, storage areas, and more. The versatility of overhead systems allows for efficient and adaptable material movement.
3. Improved Safety:
– Overhead conveyor chains minimize ground-level obstructions, reducing the risk of tripping hazards and accidents. Operators and workers can safely navigate the work area without interference from the conveyor system.
4. Product Protection:
– Overhead conveyor chains provide better protection for the products being transported. By keeping the products elevated and away from potential hazards on the floor, such as dust, debris, or spills, the risk of product damage or contamination is reduced.
5. Increased Efficiency:
– Overhead conveyor systems can enhance production efficiency by facilitating continuous material flow and reducing manual handling. They enable automated loading and unloading of materials, leading to faster processing times and improved overall productivity.
6. Easy Maintenance:
– Overhead conveyor chains are typically designed for easy maintenance. Components such as chains, trolleys, and drives can be accessed and serviced conveniently, minimizing downtime and maintenance costs.
7. Customization and Integration:
– Overhead conveyor chains can be tailored to meet specific application requirements, including load capacity, speed, and control systems. They can also be integrated with other automated systems, such as robotic workstations or sorting mechanisms, to further optimize the material handling process.
Overall, using an overhead conveyor chain system provides efficient material handling, maximizes space utilization, enhances safety, and improves productivity in industrial environments.
How does a conveyor chain handle different types of materials?
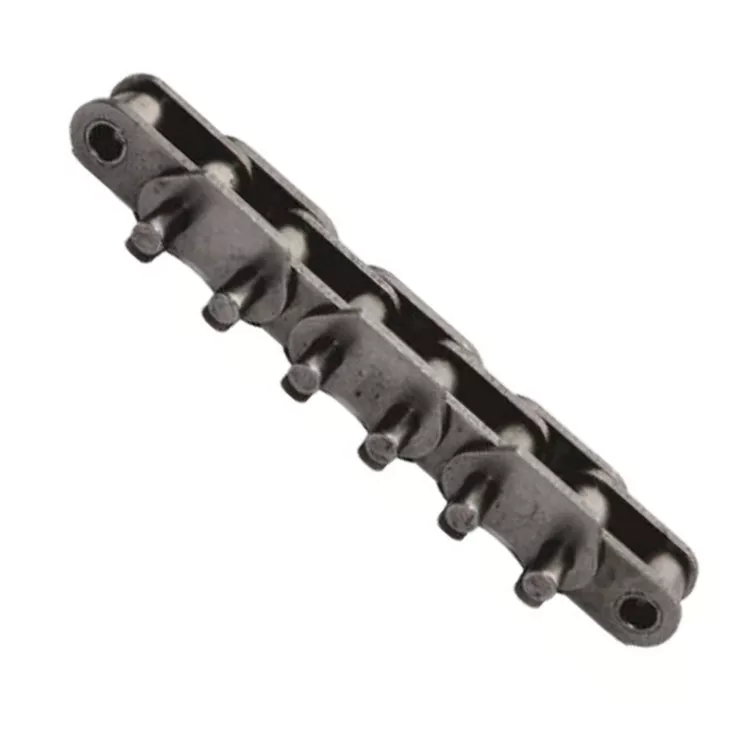
A conveyor chain is designed to handle a wide variety of materials in diverse industrial applications. It is capable of efficiently transporting different types of materials, including:
1. Bulk Materials: Conveyor chains are commonly used to handle bulk materials such as grains, coal, ores, aggregates, and powders. The design of the chain, including the spacing and shape of the links, helps prevent material spillage and ensures smooth and consistent flow.
2. Packaged Goods: Conveyor chains are also used for conveying packaged goods such as boxes, cartons, crates, and pallets. They provide a stable and reliable method of transporting these items along the production line, reducing manual handling and increasing productivity.
3. Small Parts: Conveyor chains with specialized attachments or small-pitch configurations are suitable for handling small parts or components. These chains ensure precise positioning and gentle transport of delicate or intricate items.
4. Heavy-Duty Loads: Industrial conveyor chains are capable of handling heavy-duty loads, such as automotive parts, machinery components, and large equipment. They are engineered to withstand the weight and stress of these objects, providing reliable and efficient material handling in demanding environments.
5. Food and Beverage Products: Conveyor chains used in the food and beverage industry are designed to meet strict hygiene and safety standards. They are constructed from materials that are resistant to corrosion, easy to clean, and compliant with food-grade regulations. These chains ensure the safe and contamination-free handling of food products.
6. Hazardous Materials: Conveyor chains can be used to safely transport hazardous materials, such as chemicals or waste products. Specialized chains with additional safety features, such as sealed housings or containment systems, are utilized to minimize the risk of spills or leaks.
Conveyor chains can be customized with different chain configurations, attachments, and accessories to accommodate specific material characteristics and handling requirements. The selection of the appropriate chain type, material, and design parameters ensures optimal performance and efficient material handling for a wide range of materials.
How do you optimize the efficiency of a conveyor chain system?
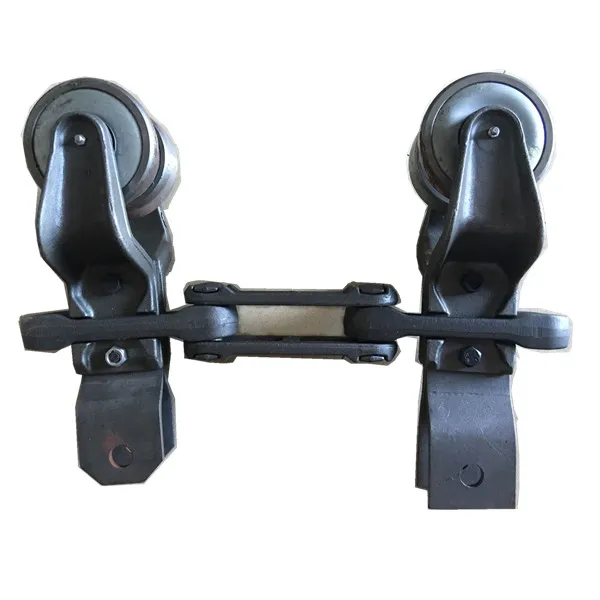
To optimize the efficiency of a conveyor chain system, several factors should be considered and implemented:
1. System Design: Ensure that the conveyor system is properly designed to minimize energy losses, reduce friction, and optimize material flow. Consider factors such as conveyor length, incline/decline angles, and the number and placement of drive units to achieve efficient operation.
2. Chain Selection: Select the appropriate conveyor chain based on the specific application requirements, such as load capacity, speed, and environmental conditions. Consider factors like chain material, pitch, and strength to ensure optimal performance and longevity.
3. Lubrication: Proper lubrication of the conveyor chain is essential for reducing friction, wear, and power consumption. Choose the right lubricant for the application and regularly maintain the lubrication levels to ensure smooth chain operation.
4. Tensioning and Alignment: Regularly inspect and adjust the tension and alignment of the conveyor chain to prevent excessive slack or tightness. Proper tensioning and alignment help to minimize chain wear, reduce energy losses, and ensure consistent performance.
5. Preventive Maintenance: Implement a regular maintenance program to identify and address potential issues before they escalate. This includes cleaning the chain, inspecting sprockets and guides, replacing worn components, and checking for proper tension and alignment. A well-maintained system reduces downtime and extends the life of the chain.
6. System Monitoring: Utilize monitoring tools such as sensors, cameras, or automated systems to track the performance of the conveyor chain system. Monitoring can provide valuable data on chain tension, alignment, speed, and power consumption, allowing for timely adjustments and optimization.
7. Training and Operator Awareness: Train operators on best practices for operating and maintaining the conveyor chain system. Promote awareness of energy efficiency, proper handling, and safety protocols to ensure optimal system performance.
By considering these factors and implementing appropriate measures, the efficiency of a conveyor chain system can be optimized, leading to improved productivity, reduced energy consumption, and longer chain life.
editor by CX 2023-11-07