Product Description
Sfr Transmission Cast Stainless Steel Plastic Double Pitch Pintle Drag Drive Roller Conveyor Chain
Products Description
Stainless steel chains are widely used in food processing, pharmaceutical, chemical production, rubber processing, non-ferrous metal smelting, electronic equipment, environmental protection equipment and heat treatment equipment and other fields of mechanical transmission and conveying equipment.
Traction chains are widely used in forklifts, CHINAMFG stackers, textile machinery, parking garages, drilling rigs, aerial work platforms, pipe benders, etc.
Drive chains are mainly used to transmit power and are widely used in agricultural machinery, construction machinery, escalator drive, logistics and packaging machinery industries.
Conveyor chain is widely used in food, wood and paper, logistics, packaging machinery, building materials machinery, environmental protection equipment and other industries for material conveying
Details Images
Agricultural Machinery Chain
Agricultural machinery chains are mainly used in rice, wheat, corn, cotton and other agricultural machinery to provide driving and conveying functions to realize the mechanization of the whole process of agricultural production from plowing, sowing to harvesting.
Conveyor chain
Conveyor chain products are characterized by high strength, wear resistance, high precision, corrosion resistance, temperature resistance, etc. to meet the needs of efficient, smooth and reliable conveying
Drive chains
The transmission chain adopts high-quality raw materials and advanced technology to develop a series of high-end chain transmission products with high wear resistance, high fatigue strength and high precision.
Product Paramenters
Company Profile
SFR Chain Group has been excelling at manufacturing and innovating motorcycle and industrial chain since 1991,always focusing on high quality and innovation to stay in the pole position of the industry.
SFR operates 4 fully owned factories and 1 joint venture, certified by ISO9002, ISO9001 and ISO/TS16949 Quality Management System.
SFR offers over 2000 series, which are exported to over 60 countries all over the World, and are widely used in variety of fields. Such as agricultural machines, motorcycles, metallurgy, wood processing, or food and beverage processing, among others. We at SFR Chain always adhere to the group’s spirit of integrity, efficiency and innovation:”We strive to offer the best products and service to our customers”
SFR is a global professional supplier focusing on chain drive solutions, with famous chain drive brands such as SFR, SUNFUN, MOTOMAX, EP and TVH.
Our commitment to R&D led SFR to establish atable cooperation with several ell-known universities and research institutes in China, as well as setting up an Intelligent Chain Drive Research Center within the group, altogether resulting in its more than 70 patents. This allows us to offer the widest range of power transmission and conveyor chain at the most competitive prices.
Since 1991, it has become a leading company in the chain industry with 5 production bases, about 110,000 square CHINAMFG of factory space, more than 180 patents, more than 2,000 chain varieties, more than 8,000 product specifications,exports to more than 80 countries worldwide. Products are widely used in many fields such as logistics and conveying, food industry, petroleum industry, engineering machinery, lifting equipment, packaging machinery processing, environmental protection equipment, tobacco machinery, etc.
Factory equipment
SFR will continue to increase the investment in manufacturing, R&D, follow the wave of Industry 4.0, continuously improve the company’s technology, product, marketing and brand power, enhance the company’s comprehensive strength, and provide customers with better chain drive solutions.
High-speed punching of industrial chain plates Automatic high-speed punching, high efficiency, high precision, and good sound insulation and environmental protection measures.
Motorcycle chain automatic assembly line The chain automatic assembly line integrates the processes of parts loading, chain assembly, automatic detection, pre-stretching, head riveting, and oiling to achieve the real automatic and efficient agricultural chain automatic assembly.
Automatic assembly line for agricultural chains Using the design of electromechanical integration, the mechanical mold and pneumatic and hydraulic parts are effectively combined together to realize the automatic assembly of complex structure chains.
Testing Machine
SFR Chain currently has 5 manufacturing plants covering over 50,000 square CHINAMFG and employing nearly 1,000 people. We bring in top talent and some of the manufacturing equipment used for manufacturing and inspection to provide the highest quality standards and create effective economies of scale.
Recommend Products
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Standard or Nonstandard: | Standard |
|---|---|
| Application: | Textile Machinery, Garment Machinery, Conveyer Equipment, Packaging Machinery, Electric Cars, Motorcycle, Food Machinery, Marine, Mining Equipment, Agricultural Machinery, Car |
| Surface Treatment: | Electroplating, Zinc Plating |
| Structure: | Roller Chain, Hollow Chain |
| Material: | Stainless Steel, Alloy |
| Type: | Roller Chain, Double Pitch Chain |
| Samples: |
US$ 2/Piece
1 Piece(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|

Can a conveyor chain be used in extreme temperature environments?
Yes, conveyor chains can be designed and manufactured to withstand extreme temperature environments. The suitability of a conveyor chain for high or low-temperature applications depends on the material composition and construction of the chain.
1. High-Temperature Environments: For applications involving high temperatures, conveyor chains made of heat-resistant materials such as stainless steel or special alloys are commonly used. These chains can withstand elevated temperatures without significant deformation or loss of strength. They are designed to resist oxidation, corrosion, and thermal expansion, ensuring reliable performance in hot environments.
2. Low-Temperature Environments: Similarly, conveyor chains can also be engineered for low-temperature applications. In cold environments, chains made of materials that remain ductile and strong at low temperatures are utilized. These chains are designed to withstand the effects of cold temperatures without becoming brittle or losing their mechanical properties.
It’s important to consult with conveyor chain manufacturers or experts who specialize in extreme temperature applications to select the most suitable chain material and design. They can provide guidance on factors such as material selection, lubrication, and operational considerations to ensure the conveyor chain performs effectively and reliably in extreme temperature environments.

Can a conveyor chain be used for heavy-duty applications?
Yes, a conveyor chain can be used for heavy-duty applications. Conveyor chains are specifically designed to handle heavy loads and provide reliable transportation in industrial environments.
Here are some factors that make conveyor chains suitable for heavy-duty applications:
1. Robust construction: Conveyor chains are typically made from high-strength materials such as alloy steel, stainless steel, or hardened carbon steel. These materials offer excellent durability and can withstand the heavy loads and harsh operating conditions commonly found in heavy-duty applications.
2. High load-carrying capacity: Conveyor chains are designed to handle significant loads, including heavy products, bulk materials, or large components. The chains are engineered with appropriate pitch, link dimensions, and strength to ensure reliable transport of heavy items.
3. Fatigue resistance: Conveyor chains are built to withstand repetitive stress and fatigue caused by continuous operation under heavy loads. They undergo specific heat treatments and surface hardening processes to enhance their resistance to wear, fatigue, and deformation.
4. Customization options: Conveyor chains can be customized to meet the specific requirements of heavy-duty applications. This includes selecting the appropriate chain type, pitch, attachment design, and surface coating for improved performance and longevity.
5. Compatibility with heavy-duty equipment: Conveyor chains are designed to integrate seamlessly with heavy-duty conveyor systems, including large motors, drives, and supporting structures. This ensures proper power transmission and smooth operation even in demanding environments.
6. Safety features: Conveyor chains for heavy-duty applications often incorporate safety features such as overload protection, emergency stops, and monitoring systems to ensure the safety of operators and prevent damage to the equipment.
It’s important to consult with a qualified engineer or conveyor manufacturer to select the appropriate conveyor chain and system components for the specific heavy-duty application. They can provide guidance on chain selection, system design, and maintenance practices to ensure optimal performance and reliability.
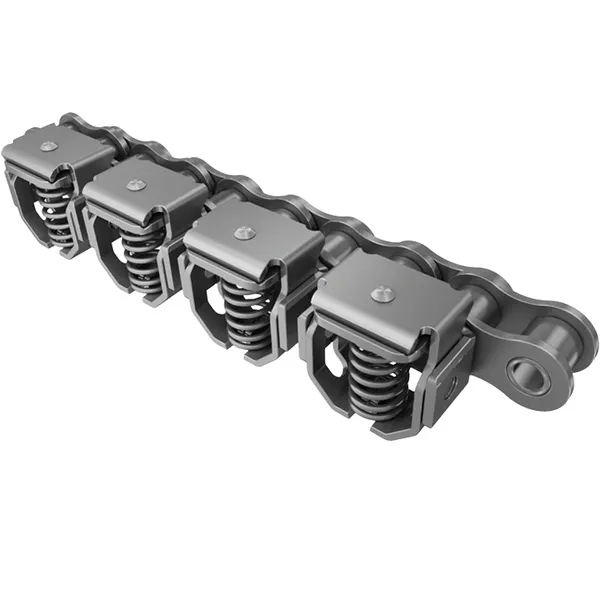
How to select the right conveyor chain for your conveyor system?
Selecting the right conveyor chain for your conveyor system is crucial to ensure optimal performance and longevity. Here are the steps to follow when choosing a conveyor chain:
- Identify your application requirements: Determine the specific requirements of your conveyor system, including the type of material being conveyed, the speed of operation, the load capacity, the environmental conditions, and any special considerations.
- Consider the chain type: Based on your application requirements, consider the different types of conveyor chains available, such as roller chains, double pitch chains, hollow pin chains, apron chains, or plastic chains. Evaluate their features and benefits to determine which type is most suitable for your needs.
- Assess the chain material: Conveyor chains are typically made from various materials such as steel, stainless steel, or plastic. Consider factors such as corrosion resistance, temperature resistance, wear resistance, and food-grade requirements when selecting the chain material.
- Determine the chain pitch: The chain pitch refers to the distance between the centers of adjacent pins. Choose the appropriate pitch size based on your conveyor system’s design, load requirements, and speed. Smaller pitch sizes provide smoother operation at higher speeds, while larger pitch sizes offer better resistance against wear and fatigue.
- Evaluate the chain strength: Consider the required tensile strength and fatigue resistance of the chain to ensure it can withstand the anticipated load and operating conditions. Factors such as chain construction, material quality, and heat treatment play a role in determining the chain’s strength.
- Consider additional features: Depending on your application, you may need additional features such as attachments, guides, or specialized coatings on the chain. Assess if any of these features are necessary to meet your specific requirements.
- Consult with experts: If you’re uncertain about the selection process or have unique application needs, it’s advisable to consult with conveyor chain manufacturers or industry experts who can provide guidance and recommendations based on their expertise.
By following these steps and carefully considering your application requirements, you can select the right conveyor chain that ensures efficient and reliable operation of your conveyor system.


editor by CX 2024-05-13
China Hot selling Stainless Steel Short Pitch Conveyor Chain with Extended Pin Short Pitch Precision Roller Chain (A series) Transmission Parts
Product Description
Stainless Steel Short Pitch Conveyor Chain With Extended Pin Short Pitch Precision Roller Chain(A series) transmission parts
We supply SS304 And SS316 Stainless Steel Conveyor Chain,Stainless Steel Conveyor Chain for Sewage, Sewage Conveyor Chain, Double conveyor chain, double pitch conveyor chain, double chain conveyor, SS conveyor chain, stainless steel conveyor chain, SS304 conveyor chain, SS316 conveyor chain, SS316L conveyor chain, sewage treatment conveyor chain, sewage disposal system chain, sewage disposal system conveyor chain, sewage treatment machine chain, sewage treatment machine conveyor chain, sewage treatment machine drive chain, sewage disposal machine chain, sewage disposal machine conveyor chain, sewage disposal machine drive chain, sewage treatment plant conveyor chain, sewage treatment plant drive chain, sewage treatment equipment conveyor chain, sewage treatment equipment drive chain
We export standard chain and also special chain as per your drawing or sample
Our stainless steel chain include:
1) Stainless steel roller chains
2) Short pitch stainless steel conveyor chain attachments
3) Double pitch stainless steel conveyor chains
4) Double pitch stainless steel conveyor chain attachments
5) Stainless steel hollow pin chains
6) Special chain as per your drawing or sample
Material: SS202, SS302, SS410, SS304, SS316, SS316L and so on
Our chain plate have special treatment and so hardness high and straightness high and tensile strength higher. We produce for famous chain factory in Europe, our quality is high, if you choose us, you choose reliable
HangZhou CHINAMFG Industry Co., Ltd. is a specialized supplier of a full range of chains, sprockets, gears, gear racks, v belt pulley, timing pulley, V-belts, couplings, machined parts and so on.
Due to our CHINAMFG in offering best service to our clients, understanding of your needs and overriding sense of responsibility toward filling ordering requirements, we have obtained the trust of buyers worldwide. Having accumulated precious experience in cooperating with foreign customers, our products are selling well in the American, European, South American and Asian markets.Our products are manufactured by modern computerized machinery and equipment. Meanwhile, our products are manufactured according to high quality standards, and complying with the international advanced standard criteria.
With many years’ experience in this line, we will be trusted by our advantages in competitive price, one-time delivery, prompt response, on-hand engineering support and good after-sales services.
Additionally, all our production procedures are in compliance with ISO9001 standards. We also can design and make non-standard products to meet customers’ special requirements. Quality and credit are the bases that make a corporation alive. We will provide best services and high quality products with all sincerity. If you need any information or samples, please contact us and you will have our soon reply.
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Usage: | Conveyor Chain |
|---|---|
| Material: | Stainless steel |
| Surface Treatment: | No |
| Customization: |
Available
| Customized Request |
|---|
.shipping-cost-tm .tm-status-off{background: none;padding:0;color: #1470cc}
| Shipping Cost:
Estimated freight per unit. |
about shipping cost and estimated delivery time. |
|---|
| Payment Method: |
|
|---|---|
|
Initial Payment Full Payment |
| Currency: | US$ |
|---|
| Return&refunds: | You can apply for a refund up to 30 days after receipt of the products. |
|---|
What are the benefits of using an overhead conveyor chain system?
Using an overhead conveyor chain system offers several benefits in various industrial applications. Here are some key advantages:
1. Space Optimization:
– Overhead conveyor chain systems utilize the vertical space, allowing efficient utilization of floor space. This is especially beneficial in facilities with limited floor area, as it enables efficient material handling and production flow without obstructing the work area.
2. Flexibility and Versatility:
– Overhead conveyor chains offer flexibility in routing and can be customized to fit the specific layout requirements of the facility. They can traverse different areas, including assembly lines, paint booths, storage areas, and more. The versatility of overhead systems allows for efficient and adaptable material movement.
3. Improved Safety:
– Overhead conveyor chains minimize ground-level obstructions, reducing the risk of tripping hazards and accidents. Operators and workers can safely navigate the work area without interference from the conveyor system.
4. Product Protection:
– Overhead conveyor chains provide better protection for the products being transported. By keeping the products elevated and away from potential hazards on the floor, such as dust, debris, or spills, the risk of product damage or contamination is reduced.
5. Increased Efficiency:
– Overhead conveyor systems can enhance production efficiency by facilitating continuous material flow and reducing manual handling. They enable automated loading and unloading of materials, leading to faster processing times and improved overall productivity.
6. Easy Maintenance:
– Overhead conveyor chains are typically designed for easy maintenance. Components such as chains, trolleys, and drives can be accessed and serviced conveniently, minimizing downtime and maintenance costs.
7. Customization and Integration:
– Overhead conveyor chains can be tailored to meet specific application requirements, including load capacity, speed, and control systems. They can also be integrated with other automated systems, such as robotic workstations or sorting mechanisms, to further optimize the material handling process.
Overall, using an overhead conveyor chain system provides efficient material handling, maximizes space utilization, enhances safety, and improves productivity in industrial environments.
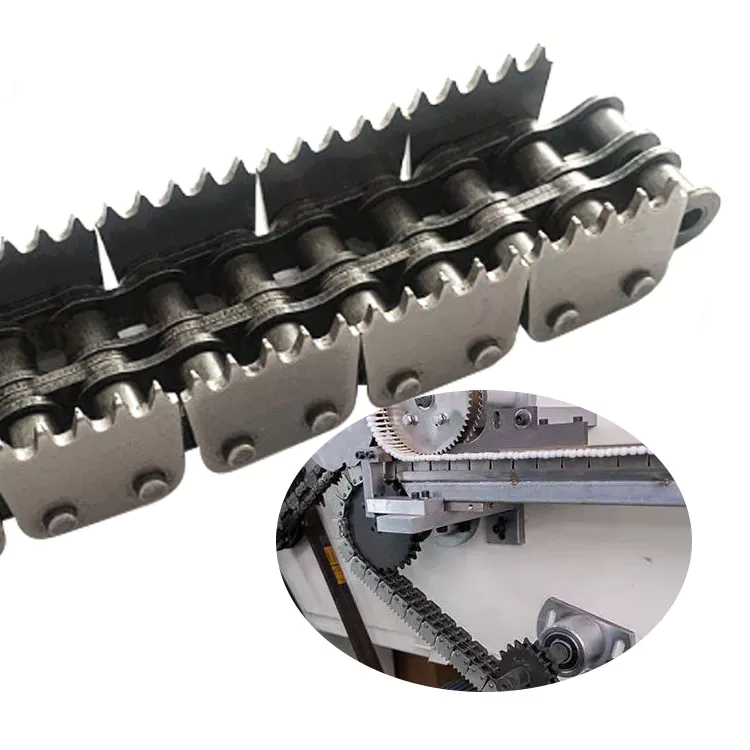
What are the different attachment options available for a conveyor chain?
Conveyor chains can be equipped with various types of attachments or accessories to accommodate specific material handling needs. Here are some common attachment options:
1. Cleats or Flights: Cleats or flights are raised sections attached to the conveyor chain to prevent materials from slipping or sliding off the chain. They are commonly used in incline or decline applications or when handling loose or bulk materials.
2. Side Plates or Side Guards: Side plates or side guards are installed along the edges of the conveyor chain to provide containment and prevent materials from spilling or falling off the sides. They are particularly useful when conveying small or irregularly shaped items.
3. Pusher Bars: Pusher bars are extensions mounted on the conveyor chain that can be pneumatically or mechanically actuated to push materials onto a different conveyor line or divert them to a specific location. They are often used for sorting or diverting applications.
4. Hold-Downs or Brackets: Hold-downs or brackets are devices attached to the conveyor chain to secure and stabilize the transported materials. They ensure that the materials remain in a fixed position during the conveying process, especially when encountering vibrations or changes in speed.
5. Guide Rails: Guide rails are installed alongside the conveyor chain to provide guidance and alignment for the materials being conveyed. They help maintain the desired path and prevent lateral movement or misalignment.
6. Magnetic Attachments: Magnetic attachments are used when handling ferrous materials. They allow the conveyor chain to attract and hold magnetic objects, ensuring effective transport and separation.
7. Tooling Plates: Tooling plates are platforms or mounting surfaces attached to the conveyor chain to accommodate specific equipment, such as fixtures, sensors, or robotic arms. They provide a convenient and customizable interface for integrating additional functionalities into the conveyor system.
8. Diverters or Transfer Units: Diverters or transfer units are specialized attachments that enable the seamless transfer of materials from one conveyor line to another, or between different processing stations. They ensure smooth transitions and precise material flow control.
These attachment options offer flexibility and versatility in conveyor chain applications, allowing customization based on the specific requirements of the material being transported or the production process. By selecting the appropriate attachments, conveyor chains can effectively handle a wide range of materials and optimize material flow within a conveyor system.
How do you calculate the required length of a conveyor chain?
Calculating the required length of a conveyor chain involves considering several factors related to the conveyor system and the specific application. Here’s a step-by-step guide:
- Determine the Conveyor Length: Measure the total length of the conveyor path, including any horizontal, inclined, or vertical sections.
- Account for Sprocket Centers: Identify the locations of the sprockets or drive units along the conveyor path. Measure the distance between each pair of adjacent sprockets.
- Calculate the Number of Links: Divide the total conveyor length by the pitch of the chain to determine the number of links required. The pitch is the distance between the center of two consecutive pins on the chain.
- Consider Tension Adjustment: Take into account any tension adjustment requirements based on the specific application. This may include allowances for tensioning devices or tension variations due to load fluctuations.
- Include End Connections: Consider the length of the end connections, such as master links or connecting pins, which are used to join the ends of the chain. Include their dimensions in the total chain length calculation.
- Add Safety Factors: Incorporate appropriate safety factors to ensure adequate chain length for proper tensioning and to accommodate any potential stretching or wear over time.
It’s important to note that the calculation of the required chain length is an estimation based on various factors and may require adjustments during the installation and tensioning process. Consulting the conveyor manufacturer’s guidelines or working with an experienced engineer can provide more precise calculations based on the specific conveyor system and application requirements.
editor by CX 2024-05-08
China Best Sales ISO 9001 Approved motorcycle part sprocket Stainless Steel Agricultural Transmission Roller conveyor Chain
Product Description
ISO 9001 Approved Agricultural Chain
Why choose us ?
1. HangZhou Xihu (West Lake) Dis.hua Chain Group Co., Ltd established in 1991, we have 5 subsidiaries in china and also have 6 subsidiaries abroad;
2. we covering a production area of 200,100 square meters, have more than 1,800 sets of advanced equipment and over 3,100 highly skilled employees, the annual production capacity has exceeded 20,000,000 meters;
3. we specialized in producing all kinds of standard chains and special chains, such as A or B series chains, drive chains, conveyor chains, drag chains, agricultural chains, sprockets, gears and so on;
4. we have obtained ISO9001, ISO14001, ISO16969, AAA and API certificates.
5. Our partners among world top enterprises, such as JOHNDEERE, NEW HOLLAND, CLAAS, HONDA, KUBOTA, YANMAR, etc.
Our agricultural chains are as following items:
1. SH series high strength heavy duty short pitch roller chains
2. SP series high strength heavy duty short pitch roller chains
3. Walking tractor chains
4. Combine chains
5. ZGS38 combine chain with attachments
6. Rice harvester chains
7. Various agricultural chain with attachments
8. S type steel agricultural chains
9. S type steel agricultural chain with attachments
10. A Type steel agricultural chains
11. CA type steel agricultural chains
12. C type steel agricultural chain with attachments
13. Special agricultural chain with attachments
1) Related Products
2) Certificates
HangZhou Xihu (West Lake) Dis.hua Chain Group Co., Ltd was founded in 1 9 9 1, and now it has five wholly owned subsidiaries, one in ZheJiang province, other four in HangZhou, ZHangZhoug province, it is a professional manufacturer of chains, sprockets, tooth gears and various power transmission products.
The group has XIHU (WEST LAKE) DIS.HUA, ZIQIANG brands, is focused on producing all variety of standard roller chains and special chains, such as conveyor chain, stainless steel chain, agricultural chain. With Xihu (West Lake) Dis.hua brand registered in more than 70 countries like America, Europe, Japan, it is building long term cooperation with these world top enterprises, such as JOHNDEERE, NEW HOLLAND, CLAAS, HONDA, KUBOTA, YANMAR.
There is a technical center of province level, Xihu (West Lake) Dis.hua academician working station, experiment station for Xihu (West Lake) Dis.hua post doctors, and national hundreds of program set up in Xihu (West Lake) Dis.hua group. With these platforms and strong technical ability, the more than hundreds of Engineers and technicians have developed all variety of special high precise and high strength products, conducted mold programs for key components in the car and national industry revitalizing program.
Great attention has been paid on environmental protection and energy saving. The product well displays environmental protection and energy saving. In the year of 2 0 0 0, Xihu (West Lake) Dis.hua took the lead in gaining I S O 1 4 0 0 1 environment management certificate and thereafter passed the inspection of clean production and recycling economy, winning the title of “ZHangZhoug Green Enterprise”.
“We are always serving our customers with our best products.”
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Usage: | Transmission Chain |
|---|---|
| Material: | Alloy/Carbon Steel |
| Surface Treatment: | Oil Blooming |
| Feature: | Heat Resistant |
| Chain Size: | 1/2"*11/128" |
| Structure: | Roller Chain |
| Customization: |
Available
| Customized Request |
|---|
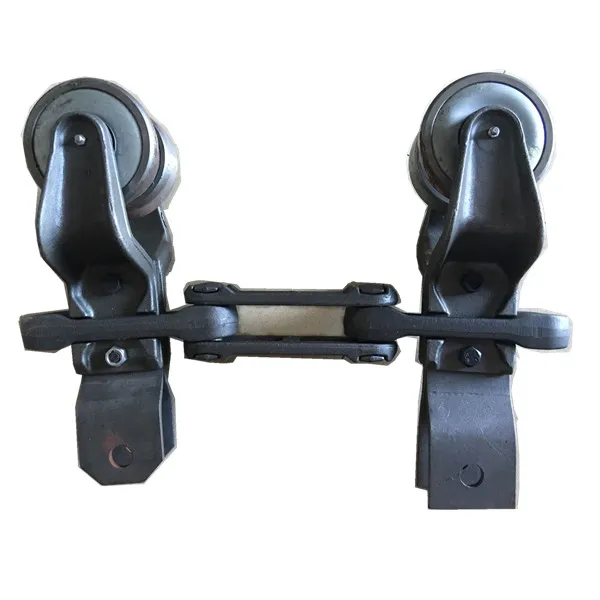
How do you calculate the required horsepower for a conveyor chain drive?
The calculation of required horsepower for a conveyor chain drive involves considering various factors related to the conveyor system and the specific application. Here is a step-by-step process:
1. Determine the Total Resistance:
– Calculate the total resistance that the conveyor chain needs to overcome during operation. This includes the resistance due to the load being conveyed, frictional losses, elevation changes, and any other resistances in the system.
2. Convert the Resistance to Equivalent Inertia:
– Convert the total resistance to an equivalent inertia by multiplying it by the square of the chain speed.
3. Calculate the Total Inertia:
– Determine the total inertia of the system by considering the inertia of all the rotating components, such as the conveyor chain, sprockets, and any other driven elements.
4. Determine the Required Torque:
– Calculate the required torque by multiplying the total inertia by the desired acceleration or deceleration rate.
5. Convert Torque to Horsepower:
– Convert the required torque to horsepower by dividing it by the motor speed (in RPM) and multiplying by a conversion factor.
6. Consider Safety Factors and Efficiency:
– Apply safety factors to the calculated horsepower to account for variations, contingencies, and future growth.
– Consider the efficiency of the drive system, including the motor, gearbox, and other transmission components, to ensure accurate power transmission.
It’s important to note that the above calculation method provides an estimate of the required horsepower. Consulting with conveyor system manufacturers, engineers, or industry-specific guidelines is recommended for precise calculations and to ensure the selected conveyor chain drive meets the application requirements.
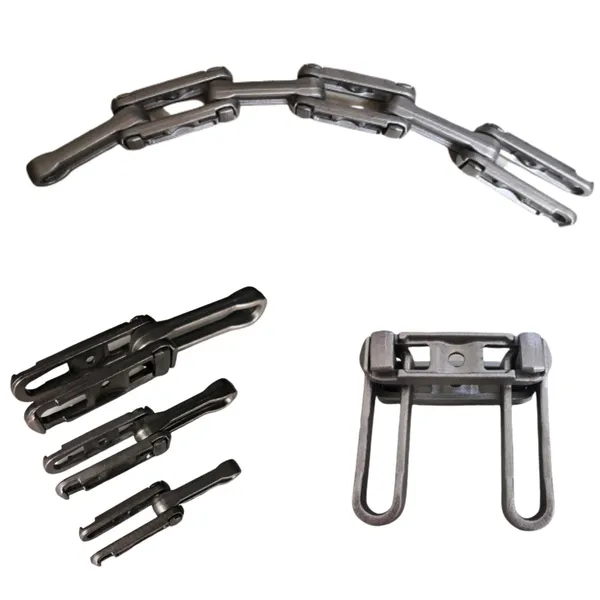
How does lubrication affect the performance of a conveyor chain?
Lubrication plays a crucial role in the performance and longevity of a conveyor chain. Proper lubrication helps to reduce friction, wear, and heat generation, ensuring smooth operation and minimizing the risk of premature failure. Here’s how lubrication affects the performance of a conveyor chain:
1. Friction Reduction: Lubrication forms a thin film between the chain components, reducing friction between metal surfaces. This reduces the energy required for operation, minimizes heat generation, and prevents excessive wear and tear.
2. Wear Prevention: Lubrication forms a protective layer on the chain components, preventing direct metal-to-metal contact. This helps to reduce wear and extend the service life of the chain.
3. Corrosion Protection: Lubricants often contain anti-corrosion additives that protect the chain from rust and oxidation. This is particularly important in environments with high humidity or exposure to corrosive substances.
4. Noise Reduction: Proper lubrication reduces the noise generated during chain operation by minimizing friction and metal-to-metal contact. This can contribute to a quieter and more comfortable working environment.
5. Temperature Control: Lubrication helps to dissipate heat generated during chain operation, preventing excessive temperature rise. This is crucial in high-speed or heavy-duty applications where heat can lead to accelerated wear and reduced chain performance.
6. Maintenance and Service Life: Regular lubrication and proper lubricant selection are essential for maintaining the chain’s performance and extending its service life. Adequate lubrication reduces the need for frequent maintenance, minimizes downtime, and lowers overall operating costs.
It’s important to follow the manufacturer’s recommendations for lubrication frequency and use the appropriate lubricant for the conveyor chain. Regular inspections and maintenance checks should also be conducted to ensure proper lubrication levels and address any issues promptly. Proper lubrication practices will enhance the performance, reliability, and durability of the conveyor chain system.
What are the different types of conveyor chains?
There are several types of conveyor chains available, each designed to meet specific application requirements. Here are some common types of conveyor chains:
- Roller chains: Roller chains are the most commonly used type of conveyor chain. They consist of a series of cylindrical rollers connected by side plates. Roller chains provide smooth and efficient movement and are suitable for medium to heavy-duty applications.
- Double pitch chains: Double pitch chains have larger pitch (distance between the centers of adjacent pins) compared to standard roller chains. They are often used in applications that require slower speeds and lighter loads.
- Hollow pin chains: Hollow pin chains have hollow pins that allow for easy attachment of various accessories or attachments. They are commonly used in conveying applications that require customization or where attachments need to be mounted.
- Apron or slat chains: Apron or slat chains consist of plates or slats that are connected by hinges. They are used in heavy-duty applications where the chain needs to support and carry large loads or withstand harsh environments.
- Plastic chains: Plastic chains are made of durable and lightweight materials such as acetal or polyethylene. They offer benefits such as corrosion resistance, low noise levels, and the ability to work in wet or washdown environments. Plastic chains are commonly used in food processing, packaging, and pharmaceutical industries.
These are just a few examples of conveyor chain types, and there are many other variations available depending on specific application requirements. The selection of the appropriate conveyor chain type depends on factors such as load capacity, speed, environment, and desired functionality.
editor by CX 2024-05-06
China Professional China Made Professional Well Performance Industrial Transmission Conveyor Roller Chain
Product Description
China Made Professional Well Performance Industrial Transmission Conveyor Roller Chain
Product Description
1. Material: Alloy steel & Stainless steel
2. Surface treatment: Shot peening / Zinc-plated / Nickel-plated / Dacromet-plated
3. Characteristic: Chain plate hole finally passed ball extrusion to ensure maximum fatigue resistance, parts of shot peening treatment makes the chain and the sleeve has a higher fatigue strength.
| Materials Available | 1. Stainless Steel: SS304, SS316, etc |
| 2. Alloy Steel: 45Mn, 42CrMo, etc | |
| 3. OEM according to your request | |
| Surface Treatment | Shot peening, Polishing, Oxygenation, Blackening, Zinc-plated, Nickel-plated, Anodized, etc. |
| Characteristic | Fire Resistant, Oil Resistant, Heat Resistant |
| Application | Agricultural machine |
| Design criterion | ISO DIN ANSI & Customer’s Drawing |
| Size | Customer’s Drawing & ISO standard |
| Package | Wooden Case / Container and pallet, or made-to-order |
| Certificate | ISO9001: 2008 |
| Advantage | First quality, best service, competitive price, fast delivery |
| Delivery Time | 20 days for samples. 45 days for official order. |
Detailed Photos
View more products,please click here…
Company Profile
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Material: | Alloy/Carbon Steel |
|---|---|
| Sample: | for Free |
| Transport Package: | Plastic Bag+Carton Box+Plywood Case |
| Specification: | S55K1, S62A2K1 |
| Trademark: | made-to-order |
| Origin: | China |
| Samples: |
US$ 0/Meter
1 Meter(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|
How do you calculate the maximum allowable tension in a conveyor chain?
The maximum allowable tension in a conveyor chain can be calculated using the following steps:
1. Determine the Chain Pitch:
– Measure the distance between the centers of two consecutive chain pins. This measurement is known as the chain pitch and is typically expressed in inches or millimeters.
2. Determine the Chain Speed:
– Determine the speed at which the conveyor chain will be operating. The chain speed is typically expressed in feet per minute or meters per second.
3. Calculate the Chain Pull:
– Determine the total weight or force that needs to be moved by the conveyor chain. This includes the weight of the conveyed material and any additional loads or forces acting on the chain.
4. Calculate the Required Tension:
– Use the following formula to calculate the required tension:
Tension = (Chain Pull × Chain Speed) / (Chain Pitch × Efficiency)
– The efficiency factor accounts for losses due to friction and other factors and is typically expressed as a decimal between 0 and 1.
5. Determine the Maximum Allowable Tension:
– The maximum allowable tension is determined by the manufacturer’s specifications for the conveyor chain. It is important to consult the manufacturer’s documentation or contact them directly to obtain the maximum allowable tension value.
6. Compare the Required Tension and Maximum Allowable Tension:
– Compare the calculated required tension with the maximum allowable tension. The required tension should be less than or equal to the maximum allowable tension to ensure safe and reliable operation of the conveyor chain.
By following these steps and considering the manufacturer’s specifications, you can accurately calculate the maximum allowable tension in a conveyor chain and ensure that it is within the safe operating limits.
What are the safety measures for working with heavy-duty conveyor chains?
Working with heavy-duty conveyor chains requires strict adherence to safety measures to protect the workers and maintain a safe working environment. Here are some important safety measures to consider:
1. Proper Training: All personnel involved in working with conveyor chains should receive comprehensive training on the safe operation and maintenance of the equipment. This includes understanding the potential hazards, safety procedures, and proper use of personal protective equipment (PPE).
2. Equipment Inspection: Regular inspection of the conveyor chain and associated components is crucial to identify any signs of wear, damage, or malfunction. This includes checking for loose fasteners, worn sprockets, misalignment, and any other potential hazards. Any issues should be addressed promptly to prevent accidents.
3. Lockout/Tagout: Before performing any maintenance or repair tasks on the conveyor chain, proper lockout/tagout procedures must be followed. This ensures that the equipment is de-energized and isolated from any power source to prevent accidental startup or movement.
4. Personal Protective Equipment (PPE): Workers should wear appropriate PPE, including safety glasses, gloves, steel-toed boots, and hearing protection. The specific PPE requirements may vary depending on the nature of the work and the potential hazards involved.
5. Safe Work Practices: Workers should follow safe work practices, such as avoiding loose clothing or jewelry that can get caught in the chain, keeping hands and clothing clear of moving parts, and using proper lifting techniques when handling heavy loads.
6. Emergency Stop Systems: Conveyor systems should be equipped with emergency stop buttons or pull cords that allow workers to quickly stop the chain in case of an emergency or hazardous situation.
7. Regular Maintenance: Scheduled maintenance and lubrication of the conveyor chain should be performed according to the manufacturer’s recommendations. This helps to ensure optimal performance and minimize the risk of unexpected failures.
8. Clear Warning Signs and Labels: Proper signage, warning labels, and safety instructions should be clearly displayed near the conveyor chain system to remind workers of potential hazards and safe operating procedures.
9. Regular Safety Training and Communication: Ongoing safety training and communication among the workforce are vital to reinforce safe practices and raise awareness of any changes or updates to safety protocols.
By implementing these safety measures and fostering a safety-conscious culture, the risks associated with working with heavy-duty conveyor chains can be minimized, ensuring the well-being of the workers and the efficient operation of the equipment.
Can a conveyor chain be used in high-temperature environments?
Yes, conveyor chains can be designed and used in high-temperature environments, but it depends on the specific type of chain and the temperature range involved. Here are some key considerations:
- Material Selection: Conveyor chains for high-temperature applications are typically made from heat-resistant materials such as stainless steel or alloy steels that can withstand elevated temperatures without significant degradation.
- Lubrication: Proper lubrication is essential in high-temperature environments to minimize friction and wear. Special high-temperature lubricants are available that can withstand the operating temperatures and provide effective chain lubrication.
- Chain Design: Chains used in high-temperature environments may have specific design features to accommodate thermal expansion and minimize the risk of binding or seizing. These can include increased clearances, special joint designs, or heat-resistant coatings.
- Temperature Limitations: Each conveyor chain has a maximum temperature limit specified by the manufacturer. It is important to consider this limit and ensure that the operating temperature does not exceed it to maintain the integrity and performance of the chain.
- Proper Maintenance: Regular inspection and maintenance are crucial in high-temperature applications. This includes monitoring chain wear, lubrication levels, and any signs of heat-induced damage or degradation.
However, it is important to note that the suitability of a conveyor chain for high-temperature environments ultimately depends on the specific operating conditions, including the temperature range, duration of exposure, and the application requirements. It is recommended to consult with the chain manufacturer or an experienced engineer to select the appropriate chain and ensure its safe and reliable operation in high-temperature environments.
editor by CX 2024-05-03
China OEM ISO DIN Standard Transmission Conveyor Drive Roller Chain for Gear Sprocket
Product Description
Welcome to visit Xihu (West Lake) Dis. CHINAMFG mechanical (chain )factory .
We produce a wide range power transmission products. Such as roller chains and leaf chains, conveyor chains, drive chains, agricultural chains .
Also we can supply all kinds of industrial sprockets, chain couplings.
Established in year of 2000. With over 20 years history of specializing in the roller chains producing. With stable and good quality. We now have gained customer’s high praise from at home and abroad.
Our manufacturing plant and workshop area is over 10000 square CHINAMFG and with staff is about 70. We are the middle scale factory in China.
Our chain quality can match with GB,DIN,ASA,ANSI,JIS standard.and have gain the ISO9001 Certificate.
Till now, except for the domestic market, we have exported many chains to USA, CANADA,COLOMBIA,BRAZIL,ARGENTINA,POLAND, ITALY,SPAIN AND SO ON.
1.Standards: ISO /DIN /ANSI/GB/JIS/ASA
2. Model: 06C-35-240, 04B-48B Simplex, Duplex, Triplex AND ACCORDING TO CUSTOMER’S REQUIREMENTS
3. Materials: Carbon steel 40Mn,# 10 FOR THE ROLLER AND BUSH,40CR FOR THE PIN
4. All spare parts of chains are heat treated(quenching and tempering) and controlled in a reasonable tolerance range and suitable for the industry standard.
5. Tensile strength: more higher than the standard about 15%
6. Certificate of Quality: ISO 9001
7. Good lubrication with excellent grease.
8. Color: Self color and shot peen.
9.Can match with sprockets freely
| we are CHINAMFG chain factory from CHINA. |
| We make roller chains over 20 years. main ASA chains: — main DIN chains:06b-08b-10b-12b-16b-20b-24b-32b main motorcycle chains: H 520 520H 530 Our quality: middle level and good and stable. Follow up XIHU (WEST LAKE) DIS.HUA standard We also exported many industrial sprockets together with our chains. We mainly exported chains to South America AND Europe. |
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Standard or Nonstandard: | Standard |
|---|---|
| Application: | Textile Machinery, Garment Machinery, Conveyer Equipment, Packaging Machinery, Electric Cars, Motorcycle, Food Machinery, Marine, Mining Equipment, Agricultural Machinery, Car |
| Surface Treatment: | Polishing |
| Structure: | Roller Chain |
| Material: | Carbon Steel |
| Type: | Short Pitch Chain |
| Samples: |
US$ 1/Meter
1 Meter(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|
How do you calculate the maximum allowable tension in a conveyor chain?
The maximum allowable tension in a conveyor chain can be calculated using the following steps:
1. Determine the Chain Pitch:
– Measure the distance between the centers of two consecutive chain pins. This measurement is known as the chain pitch and is typically expressed in inches or millimeters.
2. Determine the Chain Speed:
– Determine the speed at which the conveyor chain will be operating. The chain speed is typically expressed in feet per minute or meters per second.
3. Calculate the Chain Pull:
– Determine the total weight or force that needs to be moved by the conveyor chain. This includes the weight of the conveyed material and any additional loads or forces acting on the chain.
4. Calculate the Required Tension:
– Use the following formula to calculate the required tension:
Tension = (Chain Pull × Chain Speed) / (Chain Pitch × Efficiency)
– The efficiency factor accounts for losses due to friction and other factors and is typically expressed as a decimal between 0 and 1.
5. Determine the Maximum Allowable Tension:
– The maximum allowable tension is determined by the manufacturer’s specifications for the conveyor chain. It is important to consult the manufacturer’s documentation or contact them directly to obtain the maximum allowable tension value.
6. Compare the Required Tension and Maximum Allowable Tension:
– Compare the calculated required tension with the maximum allowable tension. The required tension should be less than or equal to the maximum allowable tension to ensure safe and reliable operation of the conveyor chain.
By following these steps and considering the manufacturer’s specifications, you can accurately calculate the maximum allowable tension in a conveyor chain and ensure that it is within the safe operating limits.
Can a conveyor chain be used in food processing applications?
Yes, a conveyor chain can be used in food processing applications. Conveyor chains play a crucial role in the efficient and hygienic handling of food products throughout the production process. Here are some key points to consider:
1. Food-Grade Materials: Conveyor chains used in food processing applications are typically made from food-grade materials such as stainless steel or plastic. These materials are corrosion-resistant, easy to clean, and comply with food safety regulations.
2. Hygiene Considerations: Food processing environments require high standards of hygiene. Conveyor chains designed for food applications incorporate features such as smooth surfaces, open link designs, and easy disassembly for thorough cleaning. They may also have specialized coatings or treatments to prevent bacterial growth.
3. Sanitary Design: Conveyor chains for food processing applications are designed with minimal crevices or joints to prevent food particles from getting trapped. They may have self-draining capabilities to remove excess fluids or debris.
4. Product Integrity: Conveyor chains in food processing applications ensure gentle handling of delicate food products to avoid damage or contamination. They can be equipped with accessories like cleats, side guards, or modular belt systems to securely hold and transport items of various shapes and sizes.
5. High Temperature and Washdown Capabilities: Some food processing applications require conveyor chains to withstand high temperatures during cooking, baking, or sterilization processes. Specialized chains with heat-resistant materials or coatings are available. Additionally, conveyor chains used in food processing should be capable of withstanding frequent washdowns and cleaning with water or cleaning agents.
6. Compliance with Standards: Conveyor chains used in food processing applications must comply with industry-specific standards such as FDA (Food and Drug Administration) regulations, HACCP (Hazard Analysis Critical Control Point) guidelines, and other food safety certifications.
When selecting a conveyor chain for food processing applications, it is important to consider the specific requirements of the production line, including the type of food being handled, the operating conditions, and the necessary sanitary standards. Proper maintenance and regular cleaning protocols should also be implemented to ensure food safety and product integrity.
How do you properly tension a conveyor chain?
Properly tensioning a conveyor chain is crucial for its smooth operation and to prevent issues like chain slipping or excessive wear. Here are the steps to properly tension a conveyor chain:
- Identify the Tensioning Points: Determine the locations where the conveyor chain can be tensioned. These are typically at the ends of the chain or at specific tensioning devices.
- Loosen the Tensioning Devices: If there are tensioning devices in place, such as adjustable bolts or tensioning screws, loosen them to allow for adjustment.
- Apply Tension: Apply tension to the conveyor chain by either manually pulling the chain or using a tensioning tool. The amount of tension required depends on the chain type and the manufacturer’s recommendations.
- Check the Tension: Use a tension gauge or other suitable method to measure the tension of the conveyor chain. The tension should fall within the specified range provided by the chain manufacturer.
- Adjust the Tension: If the tension is too loose or too tight, make adjustments accordingly. Tighten or loosen the tensioning devices until the desired tension is achieved.
- Secure the Tensioning Devices: Once the proper tension is achieved, securely tighten the tensioning devices to hold the chain in place.
- Verify the Tension: After tensioning the chain, perform a visual inspection and run the conveyor to ensure the chain runs smoothly without excessive slack or tightness. Make any further adjustments if necessary.
It’s important to refer to the specific guidelines provided by the conveyor chain manufacturer for proper tensioning instructions, as the exact method may vary depending on the chain type and design. Regularly check the tension of the conveyor chain and make adjustments as needed to maintain optimal performance.
editor by CX 2024-04-26
China best ISO Steel 08b 10b 12b 16b Conveyor Chain for Transmission
Product Description
ISO Steel 08B 10B 12B 16B Conveyor Chain for Transmission
Chain sprocket is profiled wheel with teeth that meshes with a chain, track or other perforated or indented material.
Sprockets are used in bicycles, motorcycles, cars, tanks, and other machinery.
We professionally produce different kinds of transmission sprockets, such as:
| Type | standard sprockets, standard sprockets, special sprockets, platewheel sprocket, finish bore sprocket, with bearing |
| Material | steel, stainless steel, 40CrMn |
| Surface Treatment | Blacking, zinc-plated, hardeing teeth and so on |
| Size | ISO, ANISI |
| Bore | Taper bushed bore, pilot bore, bearing bore |
All our products are produced strictly according to ISO9001 and exported to more than 50 countries.
Sprockets Feature as fiollow:
1. Material: C45, Stainless steel 304, A3 etc.
2. High precision is available as per your request.
3. Sprocket processing: Forging, cast iron, Machining(shaping, hobbing etc.)
4. Good quality with most competitive price.
5. Surface treatments such as high-frequency quenching and hardened teeth can be 40-50 HRC.
6. The special rubber can be fixed on the teeth bottom to reduce the noise and wear.
7. Standard and non-standard sprockets
Main Products:
1. Timing Belt Pulley (Synchronous Pulley), Timing Bar, Clamping Plate;
2. Forging, Casting, Stampling Part;
3. V Belt Pulley and Taper Lock Bush; Sprocket, Idler and Plate Wheel;Spur Gear, Bevel Gear, Rack;
4. Shaft Locking Device: could be alternative for Ringfeder, Sati, Chiaravalli, Tollok, etc.;
5. Shaft Coupling:including Miniature couplings, Curved tooth coupling, Chain coupling, HRC coupling, Normex coupling, Type coupling, GE Coupling, torque limiter, Universal Joint;
6. Shaft Collars: including Setscrew Type, Single Split and Double Splits;
7. Gear & Rack: Spur gear/rack, bevel gear, helical gear/rack
8. Other customized Machining Parts according to drawings (OEM).
More Advantages:
1. More competitive prices,
2. Shorter delivery date: 35 days.
3. We are the professional manufacturer in the field of Power Trans. Parts,specially for Timing Pulleys.
4. Produce standard and non-standard
5. Strict QC Management:ISO9001:2008,our engineer,Mr.Wang has specialized in the prodcution for over 20 years.
Packaging & Shipping:
All the products can be packed in cartons,or,you can choose the pallet packing.
MADE IN CHINA can be pressed on wooden cases.Land,air,sea transportation are available.UPS,DHL,TNT,
FedEx and EMS are all supported.
Company:
ZheJiang MIGHTY MACHINERY Co.Ltd., a subsidiary company of ZheJiang Machinery Imp.&Exp. Corp(SCMIEC),which is a wholly stated-owned enterprise established in1980,specialized in producing precision mechanical power transmission products. After years of hard work,Mighty become the holding company of 3 manufacturing factories and also the 1 of the largest enterprise supply power transmission parts in western China.
Mighty’s products are mainly exported to Europe,America and Middle East market. With the top-ranking management,professional technical support and abundant export experience,Mighty has established lasting and stable business partnership with many world famous companies and has got good reputation from world wide customers in international sales.
Factory View:
FAQ:
1. MOQ
A: Generally, 1 pc for standard parts; contact for nonstandard parts.
2. Delivery Time
A: In stock: within 5 working days. Out of stock: depends on your order quantity.
3. How To Select
A: part number or drawing, catalogue. If no, you can send us your sample, so we can make the drawing and sample accordingly.
4: What is the Warranty for your products?
A:Normally our warranty is 1 year.
Contacts:
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Standard or Nonstandard: | Standard |
|---|---|
| Application: | Conveyer Equipment, Motorcycle, Agricultural Machinery |
| Surface Treatment: | Shot Blasting |
| Structure: | Roller Chain |
| Material: | 40mn |
| Type: | Short Pitch Chain |
| Samples: |
US$ 0.5/Piece
1 Piece(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|
Can a conveyor chain be used in overhead conveyor systems?
Yes, a conveyor chain can be used in overhead conveyor systems. Overhead conveyor systems are designed to move materials, products, or components along an elevated path, typically in manufacturing or distribution facilities.
Conveyor chains used in overhead conveyor systems are specially designed to handle the weight and load requirements of the application. They are typically made from durable materials such as steel or stainless steel to ensure strength and longevity.
Here are some key considerations when using a conveyor chain in overhead conveyor systems:
1. Load Capacity:
– Ensure that the conveyor chain has sufficient load capacity to handle the weight of the conveyed items. The load capacity should be determined based on the maximum anticipated load and any potential dynamic forces.
2. Chain Type and Design:
– Select a conveyor chain that is suitable for overhead applications, such as an overhead conveyor chain or an inverted tooth chain. These chains are specifically designed to handle the unique requirements of overhead conveyance.
3. Lubrication:
– Proper lubrication is crucial for the smooth operation of the conveyor chain in an overhead system. Consider using lubricants that are suitable for overhead applications and ensure regular lubrication to minimize friction and wear.
4. Safety Measures:
– Implement appropriate safety measures to prevent accidents and ensure worker safety. This may include installing safety guards, emergency stop systems, and implementing regular maintenance and inspection routines.
It is important to consult with conveyor system manufacturers or experts who specialize in overhead conveyor systems to ensure the conveyor chain is selected and installed correctly for the specific application requirements.
How do you select the appropriate lubricant for a conveyor chain?
Selecting the right lubricant is crucial for maintaining the performance and longevity of a conveyor chain. Here are the key factors to consider when choosing a lubricant:
1. Chain Type and Material: Different conveyor chains may have specific requirements for lubrication based on their construction materials and design. Consult the manufacturer’s recommendations or specifications to determine the lubricant compatibility.
2. Operating Conditions: Consider the operating environment, such as temperature, humidity, and presence of contaminants. For high-temperature applications, choose a lubricant with a higher temperature tolerance. In wet or dusty environments, opt for lubricants that offer excellent resistance to water washout and provide effective protection against contaminants.
3. Load and Speed: Evaluate the load capacity and speed of the conveyor chain. Higher loads and speeds may require lubricants with better film strength and anti-wear properties to reduce friction and prevent premature wear.
4. Lubrication Method: Determine the lubrication method that will be used for the conveyor chain. Lubricants can be applied through drip systems, brushes, spray nozzles, or automatic lubrication systems. Consider the viscosity and consistency of the lubricant to ensure proper application and distribution.
5. Food-Grade Requirements: In food processing or pharmaceutical applications, where direct contact with the product may occur, it’s essential to use food-grade lubricants that meet industry regulations and requirements for safety and hygiene.
6. Maintenance Schedule: Consider the desired maintenance intervals and the lubricant’s longevity. Some lubricants may require more frequent reapplication, while others provide longer-lasting lubrication.
7. Compatibility with Other Materials: Take into account the compatibility of the lubricant with other materials in the conveyor system, such as seals, gaskets, and paints. Ensure that the lubricant does not cause any adverse effects on these components.
It is recommended to consult with lubricant manufacturers or industry experts to select the most suitable lubricant for your specific conveyor chain application. They can provide guidance based on their expertise and knowledge of lubricant formulations and performance characteristics.
What are the industry standards and regulations for conveyor chains?
In the field of conveyor chains, there are several industry standards and regulations that help ensure safety, performance, and quality. Some of the commonly recognized standards include:
1. ISO 1977:2013 – Conveyor chains, attachments, and sprockets: This International Organization for Standardization (ISO) standard specifies the requirements and dimensions for various types of conveyor chains, attachments, and sprockets used in general industrial applications.
2. ANSI/ASME B29.1 – Precision Power Transmission Roller Chains, Attachments, and Sprockets: This American National Standard Institute (ANSI) standard provides guidelines for the design, dimensions, and performance of roller chains, attachments, and sprockets used in power transmission systems, including conveyor chains.
3. CEMA – Conveyor Equipment Manufacturers Association: CEMA publishes various standards and technical documents related to conveyor systems, including conveyor chains. These standards cover topics such as safety, design, installation, maintenance, and operation of conveyor equipment.
4. OSHA – Occupational Safety and Health Administration: OSHA is a regulatory agency in the United States that sets and enforces safety standards for workplaces. They have specific regulations related to conveyor systems, including requirements for guarding, maintenance, and employee safety.
5. Local and National Building Codes: Depending on the location and application, there may be specific building codes or regulations that dictate the design, installation, and operation of conveyor chains. These codes ensure compliance with safety and structural requirements.
It’s important for conveyor chain manufacturers, system integrators, and end-users to adhere to these industry standards and regulations to ensure the safe and reliable operation of conveyor systems. Compliance with these standards helps to maintain worker safety, promote system performance, and ensure compatibility and interchangeability of conveyor chain components.
editor by CX 2024-04-25
China Professional ISO 9001 Approved motorcycle part sprocket Stainless Steel Agricultural Transmission Roller conveyor Chain
Product Description
ISO 9001 Approved Agricultural Chain
Why choose us ?
1. HangZhou Xihu (West Lake) Dis.hua Chain Group Co., Ltd established in 1991, we have 5 subsidiaries in china and also have 6 subsidiaries abroad;
2. we covering a production area of 200,100 square meters, have more than 1,800 sets of advanced equipment and over 3,100 highly skilled employees, the annual production capacity has exceeded 20,000,000 meters;
3. we specialized in producing all kinds of standard chains and special chains, such as A or B series chains, drive chains, conveyor chains, drag chains, agricultural chains, sprockets, gears and so on;
4. we have obtained ISO9001, ISO14001, ISO16969, AAA and API certificates.
5. Our partners among world top enterprises, such as JOHNDEERE, NEW HOLLAND, CLAAS, HONDA, KUBOTA, YANMAR, etc.
Our agricultural chains are as following items:
1. SH series high strength heavy duty short pitch roller chains
2. SP series high strength heavy duty short pitch roller chains
3. Walking tractor chains
4. Combine chains
5. ZGS38 combine chain with attachments
6. Rice harvester chains
7. Various agricultural chain with attachments
8. S type steel agricultural chains
9. S type steel agricultural chain with attachments
10. A Type steel agricultural chains
11. CA type steel agricultural chains
12. C type steel agricultural chain with attachments
13. Special agricultural chain with attachments
1) Related Products
2) Certificates
HangZhou Xihu (West Lake) Dis.hua Chain Group Co., Ltd was founded in 1 9 9 1, and now it has five wholly owned subsidiaries, one in ZheJiang province, other four in HangZhou, ZHangZhoug province, it is a professional manufacturer of chains, sprockets, tooth gears and various power transmission products.
The group has XIHU (WEST LAKE) DIS.HUA, ZIQIANG brands, is focused on producing all variety of standard roller chains and special chains, such as conveyor chain, stainless steel chain, agricultural chain. With Xihu (West Lake) Dis.hua brand registered in more than 70 countries like America, Europe, Japan, it is building long term cooperation with these world top enterprises, such as JOHNDEERE, NEW HOLLAND, CLAAS, HONDA, KUBOTA, YANMAR.
There is a technical center of province level, Xihu (West Lake) Dis.hua academician working station, experiment station for Xihu (West Lake) Dis.hua post doctors, and national hundreds of program set up in Xihu (West Lake) Dis.hua group. With these platforms and strong technical ability, the more than hundreds of Engineers and technicians have developed all variety of special high precise and high strength products, conducted mold programs for key components in the car and national industry revitalizing program.
Great attention has been paid on environmental protection and energy saving. The product well displays environmental protection and energy saving. In the year of 2 0 0 0, Xihu (West Lake) Dis.hua took the lead in gaining I S O 1 4 0 0 1 environment management certificate and thereafter passed the inspection of clean production and recycling economy, winning the title of “ZHangZhoug Green Enterprise”.
“We are always serving our customers with our best products.”
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Usage: | Transmission Chain |
|---|---|
| Material: | Alloy/Carbon Steel |
| Surface Treatment: | Oil Blooming |
| Feature: | Heat Resistant |
| Chain Size: | 1/2"*11/128" |
| Structure: | Roller Chain |
| Customization: |
Available
| Customized Request |
|---|
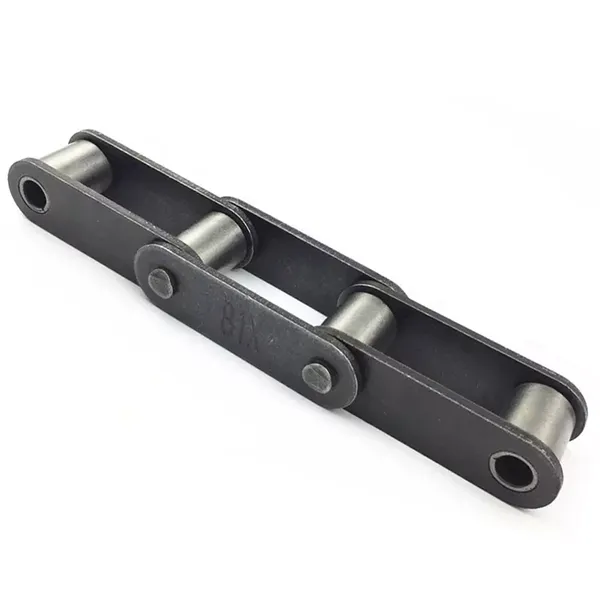
How does a conveyor chain handle accumulation and indexing applications?
In conveyor systems, accumulation and indexing refer to specific methods of controlling the movement and positioning of items along the conveyor line. A conveyor chain can effectively handle these applications through the use of specialized components and control mechanisms. Here’s a detailed explanation:
Accumulation:
– Accumulation refers to the process of temporarily storing or buffering items on the conveyor to control the flow of materials. Conveyor chains designed for accumulation applications typically incorporate features such as low-friction chain guides, accumulating zones, and sensors.
– In an accumulation conveyor chain system, the chain is divided into discrete zones where items can accumulate. As products enter a zone, the chain slows down or stops, allowing items to accumulate without colliding with each other. Sensors or photoelectric cells detect the presence of items in each zone and provide signals to control the chain movement.
– The accumulation zones in the conveyor chain system can be controlled in different ways, such as through the use of motorized rollers, pneumatic devices, or electronic sensors. This ensures a controlled and synchronized flow of items along the conveyor line.
Indexing:
– Indexing refers to the precise positioning of items at specific intervals along the conveyor line. This is commonly used in applications where accurate positioning or sequencing is required, such as assembly or packaging processes.
– Conveyor chains designed for indexing applications incorporate specialized index pins, stops, or precision indexing drives. These components work together to accurately position items at predetermined locations along the conveyor.
– The indexing mechanism of a conveyor chain system can be driven by mechanical cams, servo motors, or programmable logic controllers (PLCs). The indexing motion can be synchronized with other processes or machines downstream to ensure precise assembly or packaging operations.
– By combining accumulation and indexing capabilities, a conveyor chain system can handle a wide range of applications, including sorting, buffering, sequencing, and automated assembly. It provides control over the flow and positioning of items, allowing for efficient material handling and optimized production processes.
Can a conveyor chain be used in food processing applications?
Yes, a conveyor chain can be used in food processing applications. Conveyor chains play a crucial role in the efficient and hygienic handling of food products throughout the production process. Here are some key points to consider:
1. Food-Grade Materials: Conveyor chains used in food processing applications are typically made from food-grade materials such as stainless steel or plastic. These materials are corrosion-resistant, easy to clean, and comply with food safety regulations.
2. Hygiene Considerations: Food processing environments require high standards of hygiene. Conveyor chains designed for food applications incorporate features such as smooth surfaces, open link designs, and easy disassembly for thorough cleaning. They may also have specialized coatings or treatments to prevent bacterial growth.
3. Sanitary Design: Conveyor chains for food processing applications are designed with minimal crevices or joints to prevent food particles from getting trapped. They may have self-draining capabilities to remove excess fluids or debris.
4. Product Integrity: Conveyor chains in food processing applications ensure gentle handling of delicate food products to avoid damage or contamination. They can be equipped with accessories like cleats, side guards, or modular belt systems to securely hold and transport items of various shapes and sizes.
5. High Temperature and Washdown Capabilities: Some food processing applications require conveyor chains to withstand high temperatures during cooking, baking, or sterilization processes. Specialized chains with heat-resistant materials or coatings are available. Additionally, conveyor chains used in food processing should be capable of withstanding frequent washdowns and cleaning with water or cleaning agents.
6. Compliance with Standards: Conveyor chains used in food processing applications must comply with industry-specific standards such as FDA (Food and Drug Administration) regulations, HACCP (Hazard Analysis Critical Control Point) guidelines, and other food safety certifications.
When selecting a conveyor chain for food processing applications, it is important to consider the specific requirements of the production line, including the type of food being handled, the operating conditions, and the necessary sanitary standards. Proper maintenance and regular cleaning protocols should also be implemented to ensure food safety and product integrity.
How do you properly tension a conveyor chain?
Properly tensioning a conveyor chain is crucial for its smooth operation and to prevent issues like chain slipping or excessive wear. Here are the steps to properly tension a conveyor chain:
- Identify the Tensioning Points: Determine the locations where the conveyor chain can be tensioned. These are typically at the ends of the chain or at specific tensioning devices.
- Loosen the Tensioning Devices: If there are tensioning devices in place, such as adjustable bolts or tensioning screws, loosen them to allow for adjustment.
- Apply Tension: Apply tension to the conveyor chain by either manually pulling the chain or using a tensioning tool. The amount of tension required depends on the chain type and the manufacturer’s recommendations.
- Check the Tension: Use a tension gauge or other suitable method to measure the tension of the conveyor chain. The tension should fall within the specified range provided by the chain manufacturer.
- Adjust the Tension: If the tension is too loose or too tight, make adjustments accordingly. Tighten or loosen the tensioning devices until the desired tension is achieved.
- Secure the Tensioning Devices: Once the proper tension is achieved, securely tighten the tensioning devices to hold the chain in place.
- Verify the Tension: After tensioning the chain, perform a visual inspection and run the conveyor to ensure the chain runs smoothly without excessive slack or tightness. Make any further adjustments if necessary.
It’s important to refer to the specific guidelines provided by the conveyor chain manufacturer for proper tensioning instructions, as the exact method may vary depending on the chain type and design. Regularly check the tension of the conveyor chain and make adjustments as needed to maintain optimal performance.
editor by CX 2024-04-16
China Professional Bucket Elevator Transmission Chain Conveyor Bucket Chain Nse100
Product Description
HangZhou HAYING TECHNOLOGY INDUSTRIES CO., LTD
We are a research and development production, distribution in 1 of the business enterprises. The main production of Marine anchor chain and hoist ring chain, hoist chain and various accessories.
Founded in 1965, has been producing Marine anchor chain (13-46) and elevator ring chain (13-30), plate chain and various types of machine accessories. Also distributes Japanese standard, American standard, German standard series chain, sprocket, can be processed according to the user’s drawing.
Products are widely used in agricultural machinery, lifting platform, food machinery, metallurgical machinery, mining machinery, engineering machinery, road construction machinery, CNC machinery and other industries.
Our high-quality products have won the recognition of the majority of users, the current products are not only sold to more than 30 provinces and cities in the country, but also exported to many countries in Asia, Europe and America.
Our company has a complete and scientific quality management system, we regard quality as the core element of the long-term development of enterprises. And has a mature production technology, good service attitude of the team. We will continue to strengthen the technology research and development and manufacturing capabilities of high-end products, and continue to introduce products with market competitiveness to meet the needs of our customers.
Product Description
Large conveying capacity: conveying capacity up to 100m3/h
Long service life: The high strength wear-resistant chain made of alloy steel by advanced heat treatment means can ensure the service life of the conveyor chain for 3-5 years under normal continuous use
Wide lifting range: it can not only lift powder and granular materials, but also lift large grinding materials and materials with temperatures up to 200ºC
High lifting height: under the rated conveying capacity, the lifting height can reach 50m. Materials with high humidity and strong viscosity should not be selected
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Material: | Iron |
|---|---|
| Structure: | Welded Chain |
| Surface Treatment: | Polishing |
| Chain Size: | 1/2"*11/128" |
| Feature: | Heat Resistant |
| Transport Package: | Wooden Box |
| Customization: |
Available
| Customized Request |
|---|
How do you calculate the chain pull force in a conveyor chain system?
The chain pull force, also known as the chain tension, is an important parameter to determine in a conveyor chain system. It represents the force required to move the conveyed load along the conveyor. The calculation of chain pull force involves several factors:
1. Weight of the Load: Determine the weight of the load being conveyed. This includes the weight of the product, packaging materials, and any additional equipment or components carried by the conveyor.
2. Friction Coefficients: Identify the friction coefficients between the load and the conveyor components. This includes the friction between the product and the conveyor chain, as well as the friction between the product and the conveyor bed or guides. These coefficients are typically provided by the manufacturer or can be obtained through testing.
3. Incline or Decline Angle: Consider the angle at which the conveyor operates. If the conveyor has an incline or decline, the angle will affect the force required to move the load.
4. Acceleration and Deceleration: Account for any acceleration or deceleration requirements in the conveyor system. If the conveyor needs to start or stop abruptly or if there are changes in speed, these factors will impact the chain pull force.
Once these factors are determined, the chain pull force can be calculated using the following formula:
Chain Pull Force = (Weight of Load + Friction Force) × (1 + Incline or Decline Factor) × (1 + Acceleration or Deceleration Factor)
It’s important to note that the accuracy of the calculation depends on the accuracy of the input values. Therefore, it’s recommended to consult the conveyor manufacturer or an engineering professional to ensure precise calculations and proper sizing of the conveyor chain.
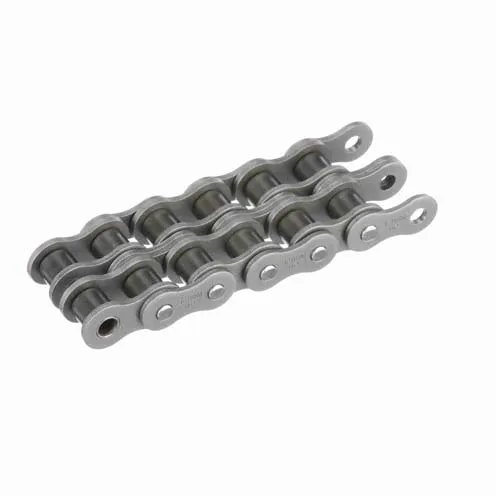
What are the benefits of using a modular conveyor chain system?
A modular conveyor chain system offers several benefits in terms of flexibility, efficiency, and ease of maintenance. Here are some key advantages:
1. Versatility: Modular conveyor chains are designed with interlocking modules that can be easily connected and disconnected. This allows for flexibility in configuring the conveyor system according to specific layout requirements, production needs, or space limitations. Modules can be added, removed, or repositioned to accommodate changing production processes or product variations.
2. Customizability: The modular design of the conveyor chain system enables customization to meet specific application requirements. Different types of modules are available, including straight sections, curves, inclines, declines, merges, and diverters. Accessories such as side guides, cleats, or product hold-downs can be easily integrated into the system.
3. Quick Installation and Modification: Modular conveyor chains are designed for easy installation and modification. With their snap-in or snap-on connections, modules can be rapidly assembled or disassembled, reducing downtime during system setup or reconfiguration. This feature also facilitates maintenance, repairs, or future expansions.
4. Enhanced Efficiency: The modularity of the conveyor chain system allows for efficient material handling and optimized workflow. The smooth transfer between modules minimizes product jams or misalignments, ensuring a continuous and consistent flow of materials. The ability to incorporate curves or inclines in the system enables efficient use of floor space and facilitates the movement of products through different elevations.
5. Easy Maintenance: Modular conveyor chain systems are designed for ease of maintenance. Individual modules can be easily accessed and replaced without disassembling the entire system. This reduces maintenance time and costs. Additionally, the open structure of the modules allows for easy cleaning, debris removal, and inspection.
6. Durability and Reliability: Modular conveyor chains are typically made from high-quality materials such as plastic or stainless steel, ensuring durability and long-lasting performance. They are resistant to wear, corrosion, and chemical damage, making them suitable for various industrial environments. The interlocking design provides stability and prevents chain slippage during operation.
7. Safety Features: Modular conveyor chain systems can incorporate safety features such as emergency stop buttons, safety guarding, or sensors for detecting blockages or excessive loads. These features help maintain a safe working environment for operators and protect the integrity of the products being transported.
Overall, a modular conveyor chain system offers versatility, customizability, efficiency, and ease of maintenance. It is a reliable solution for material handling in industries such as manufacturing, packaging, distribution, and logistics.
What safety precautions should be followed when working with conveyor chains?
Working with conveyor chains involves potential hazards, and it is essential to follow proper safety precautions to ensure the well-being of workers and prevent accidents. Here are some important safety measures to consider:
- Proper Training: Ensure that workers operating or maintaining conveyor chains receive proper training on safe practices, including chain handling, maintenance procedures, and emergency protocols.
- Personal Protective Equipment (PPE): Workers should wear appropriate PPE, such as safety glasses, gloves, and steel-toed shoes, to protect themselves from potential hazards, including flying debris, pinch points, or entanglement.
- Lockout/Tagout: Before performing any maintenance or repair tasks on conveyor chains, follow lockout/tagout procedures to isolate and de-energize the equipment to prevent accidental startup or release of stored energy.
- Guarding: Ensure that conveyor chains are adequately guarded to prevent access to moving parts, such as pinch points and rotating sprockets. Guards should be securely in place and not interfere with the chain’s operation.
- Housekeeping: Keep the work area clean and free of debris, tools, or other objects that could cause tripping hazards or interfere with the operation of the conveyor chain.
- Regular Inspections: Regularly inspect the conveyor chains for any signs of wear, damage, or misalignment. Address any issues promptly to prevent potential safety hazards.
- Safe Loading and Unloading: When loading or unloading materials onto the conveyor, follow safe lifting techniques and ensure the load is evenly distributed to prevent overloading or imbalance.
- Emergency Stop Devices: Install and clearly mark emergency stop devices along the conveyor system to enable immediate shutdown in case of an emergency or hazardous situation.
- Clear Communication: Establish clear communication protocols, including signals or signs, to ensure effective communication between workers operating different sections of the conveyor system.
These safety precautions are general guidelines, and it’s important to consult and adhere to specific safety regulations and guidelines provided by the equipment manufacturer and relevant safety authorities. Regular safety training, awareness, and a proactive safety culture are crucial in maintaining a safe working environment when working with conveyor chains.
editor by CX 2024-04-02
China manufacturer Abg2820 Drive Chain 16b-1*56L 54749486 Auger Transmission Chain
Product Description
Detailed Photos
Company Profile
HangZhou CHINAMFG Machinery Technology Co.Ltd is specilized in manufacturing and distributing road equipments spare parts for over 10 years.We offer over 85% CHINAMFG spare parts for various brand of road equipments like Vogele, Hamm, Bomag, ABG, Dynapac, Roadtec, etc.With the advanced technical support from Germany, CHINAMFG is always Focusing on products development and market testing.Now the products quality is catching up the international standard and winning the trust of customersAll over USA, North Europe, East Europe, Southeast Asia, Australia, Middle east,etc.And we always continue to offer stable and reliable quality products, advanced technical support and professional service.We are going stronger with the support of all our dear customers.
Packaging & Shipping
1. Delivery terms:by sea/ by air
2. Delivery times:7-15 Days
3. Payment terms:FOB/EXW/CIF
Our Services
1. Warranty
2. After-sales service
3. Quality certification
4. Customized service
5. Sample service
/* January 22, 2571 19:08:37 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| After-sales Service: | Aftersales Services Available |
|---|---|
| Warranty: | One Year or 2000 Working H |
| Type: | Transmission Chain |
| Application: | Conveyor System |
| Condition: | New |
| Delivery Term: | EXW/Fob/CIF |
| Samples: |
US$ 71/Piece
1 Piece(Min.Order) | |
|---|
What are the benefits of using a self-lubricating conveyor chain?
Self-lubricating conveyor chains offer several advantages over traditional lubricated chains. Here are some key benefits:
1. Reduced Maintenance: Self-lubricating chains eliminate the need for regular lubrication, reducing the time and effort required for maintenance. This is particularly beneficial in applications where access to the chain is difficult or time-consuming.
2. Cost Savings: By eliminating the need for external lubrication, self-lubricating chains can help reduce lubrication costs over the lifetime of the chain. This includes the cost of lubricants, as well as the labor and equipment required for lubrication maintenance.
3. Clean and Environmentally Friendly: Self-lubricating chains do not require external lubricants, resulting in a cleaner working environment. There is no risk of lubricant spills or contamination of the surrounding area, making them ideal for applications that require strict cleanliness standards, such as food processing or pharmaceutical industries.
4. Extended Chain Life: Self-lubricating chains are designed with built-in lubrication systems that provide a continuous and controlled supply of lubricant to the chain components. This helps reduce friction, wear, and heat generation, resulting in longer chain life and improved performance.
5. Improved Reliability: With consistent and reliable lubrication, self-lubricating chains maintain optimal performance and minimize the risk of chain failure or breakdown. They are less susceptible to premature wear, elongation, and corrosion, ensuring a more reliable and efficient conveyor system.
It’s important to note that the specific benefits of self-lubricating chains may vary depending on the manufacturer and the design of the chain. It’s recommended to consult with the chain manufacturer or an industry expert to understand the suitability and advantages of self-lubricating chains for a particular application.
What are the advantages of using a plastic conveyor chain?
Plastic conveyor chains offer several advantages over traditional metal chains. Here are some of the key advantages:
1. Corrosion Resistance: Plastic chains are highly resistant to corrosion, making them ideal for applications in humid or corrosive environments. They do not rust or deteriorate when exposed to moisture or chemicals.
2. Lightweight: Plastic chains are significantly lighter than metal chains, making them easier to handle and install. Their lightweight nature reduces the overall weight of the conveyor system and can result in energy savings during operation.
3. Low Noise Operation: Plastic chains generate less noise compared to metal chains, leading to a quieter working environment. This can be particularly beneficial in industries where noise reduction is important, such as food processing or packaging.
4. Reduced Friction and Wear: Plastic chains have self-lubricating properties, which reduce friction and wear. This results in lower maintenance requirements and longer chain life. The smooth surface of plastic chains also minimizes the risk of product damage during transportation.
5. Flexibility and Modularity: Plastic chains can be easily customized and designed to fit specific conveyor system requirements. They offer flexibility in terms of length, width, and configuration. Additionally, plastic chains are often modular, allowing for easy replacement of damaged or worn-out sections without replacing the entire chain.
6. Cost-Effective: Plastic conveyor chains are generally more cost-effective compared to metal chains. They are often less expensive to manufacture and offer a longer lifespan with minimal maintenance requirements, resulting in lower overall costs.
7. Chemical Resistance: Plastic chains are resistant to a wide range of chemicals, making them suitable for applications where exposure to aggressive substances is a concern. They can withstand contact with oils, acids, alkalis, and various cleaning agents.
Overall, the advantages of using a plastic conveyor chain include corrosion resistance, lightweight design, low noise operation, reduced friction and wear, flexibility, cost-effectiveness, and chemical resistance. These benefits make plastic chains a popular choice in various industries, including food processing, packaging, pharmaceuticals, and logistics.

What are the cost considerations when purchasing a conveyor chain?
When purchasing a conveyor chain, there are several cost considerations that need to be taken into account to ensure an optimal investment and operational efficiency.
1. Initial Cost: The initial cost of the conveyor chain includes the cost of the chain itself, as well as any additional components such as sprockets, attachments, and connecting links. It is important to compare prices from different suppliers and evaluate the overall value for the money.
2. Maintenance and Repair Costs: Consider the long-term maintenance and repair costs associated with the conveyor chain. Some chains may require more frequent lubrication or replacement of components, which can add to the overall operating expenses.
3. Service Life: The service life of the conveyor chain is an essential factor in determining its cost-effectiveness. Chains with longer service life may have a higher initial cost but can result in lower replacement and downtime costs in the long run.
4. Energy Efficiency: Energy consumption is an ongoing cost to consider. Conveyor chains that offer lower friction and efficient power transmission can contribute to energy savings and reduce operating expenses.
5. Maintenance Ease: Consider the ease of maintenance when selecting a conveyor chain. Chains that are easier to clean, inspect, and maintain can reduce labor costs and increase operational efficiency.
6. Compatibility and Integration: Ensure that the selected conveyor chain is compatible with the existing conveyor system or equipment. Retrofitting or modifying the system to accommodate a specific chain may incur additional costs.
7. Supplier Support and Warranty: Evaluate the level of technical support provided by the supplier and the warranty coverage offered for the conveyor chain. This can impact the overall cost of ownership and provide peace of mind in case of any unforeseen issues.
It is important to consider these factors holistically and make a cost-benefit analysis based on the specific requirements of the application. Choosing a conveyor chain that aligns with the budget, performance needs, and long-term cost considerations will help optimize the investment and ensure efficient material handling operations.
editor by CX 2024-03-28
China OEM Stainless Steel Maintenance Free Agricultural Machnery Conveyor Link Durable Transmission Roller Chain
Product Description
Company Profile
-HangZhou CHOHO Industrial Co., Ltd. was founded in 1999. Has become the leader of chain system technology, the first batch of natioal recognized enterprise technology center,national technology innovation demonstration enterprise,and the first A-share listed company in China’s chain drive industry.The securities code is 003033.
-CHOHO has 4 subsidiaries, including testing technology and international trading companies. has 4 factories in HangZhou, Thailand factory, ZheJiang R&D Center and Tokyo R&D Center. In addition, CHOHO ZHangZhoug Industrial zone is expected to be completed & put into operation next year.
-We specialized in producing all kinds of standard chains and special chains, such as Agricultural Chain, Sprocket, Chain Harrow, Tillage Parts,Rice Harvester Chain, GS38 Chain, Roller Chain, Automobile Chain, Motorcycle Chain Industrial Chain and so on.Our partners among world top enterprises, such as LOVOL,JOHN DEERE,NEW HOLLAND, CLASS,AGCO,DEUTZFAHR,HONDA, KUBOTA etc.
Production Capacity Equipment
By 2571,CHOHO has more than 2,700 sets of main production equipment and more than 600 sets of high-precision equipment,With the domestic advanced product laboratory and chain production assembly line, CHOHO has strong research and development and testing capabilities for high-end chain products.
Our Advantages
1. Any inquiry you make will be answered professionally within 6~8 hours.
2. Attaches great importance to product quality and approved by many global quality system certification,such as France, Norway, Germany.
3. Focused on Chain since 1999, have rich experience in Production.
4. High-quality workers,First-class advanced equipment,good quality control,advanced technology.
5. Be Good at Custom-Made Products, provide customized services for customers.
6. Participated in the drafting of 24 national and industrial standards such as chains.As of 2571-Mar, CHOHO has 180 authorized patents.
7. With the responsibility of “Providing high quality chain system with the same service life for the global locomotive industry”, have established a strong R&D team.
CHOHO has a natural brand awareness. As of January 2571, CHOHO has registered the “CHOHO” trademark in more than 60 countries, including the United States, Japan, the United Kingdom, France, Germany, Russia, Spain, Austria, Belgium, Bulgaria, Croatia, Czech Republic, Denmark, Finland, Greece , Hungary, Ireland, Italy, Netherlands, Poland, Portugal, Romania, Ukraine, Sweden, Australia, Algeria, Egypt, Kenya, Morocco, South Korea, Kazakhstan, Mongolia, Syria, Thailand, Pakistan, India, Brazil, Mexico, Colombia, etc.
Product Advantages
Certifications
CHOHO attaches great importance to product quality and approved by many global quality system certification, such as France, Norway, and Germany. Through the establishment of a sophisticated production management process and quality control system, the entire product process control is achieved. With the introduction of advanced production, processing, and testing equipment, CHOHO has internationally leading full-process quality control capabilities to provide customers with high-quality products.
Choho Provide Chain System Solutions for The Global Top 500 and The Enterprises in Various Fields Top 10!
Broad Customer Channels Market Continues to Develop!
CHOHO has been invited to participate in domestic & international agricultural machinery exhibitions, such as Hannover Messe, Bologna Fair, Canton Fair ,VIV ASIA and so on!
Packaging & Shipping
| Packaging Details: | Chain+Plastic Bag+Neutral Box+Wooden case+Big Carton+Steel Pallets or Customization |
FAQ
1. Are you manufacturer or trade Company?
We are a factory focused on producing and exporting Chain over 23 years,have a professional international trade team.
2. What terms of payment you usually use?
T/T 30% deposit and 70% against document, L/C at sight
3. What is your lead time for your goods?
Normally 30~45 days.Stock can be shipped immediately.
4. Do you attend any Show?
We attend Hannover show in Germany, EIMA in Italy, CHINAMFG in France, CIAME in China and many other Agricultural machinery shows.
5.Do you offer free samples?
Yes,we can.or you just bear the shipping cost.
6.Is OEM available?
Yes, OEM is available. We have professional designers to help you design.
/* March 10, 2571 17:59:20 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Usage: | Transmission Chain, Conveyor Chain, Dedicated Special Chain, Maintenance Free Chain |
|---|---|
| Material: | Stainless steel |
| Surface Treatment: | Polishing |
| Samples: |
US$ 1/Meter
1 Meter(Min.Order) | Order Sample Sample
|
|---|
| Customization: |
Available
| Customized Request |
|---|
.shipping-cost-tm .tm-status-off{background: none;padding:0;color: #1470cc}
|
Shipping Cost:
Estimated freight per unit. |
about shipping cost and estimated delivery time. |
|---|
| Payment Method: |
|
|---|---|
|
Initial Payment Full Payment |
| Currency: | US$ |
|---|
| Return&refunds: | You can apply for a refund up to 30 days after receipt of the products. |
|---|
How do you calculate the maximum allowable tension in a conveyor chain?
The maximum allowable tension in a conveyor chain can be calculated using the following steps:
1. Determine the Chain Pitch:
– Measure the distance between the centers of two consecutive chain pins. This measurement is known as the chain pitch and is typically expressed in inches or millimeters.
2. Determine the Chain Speed:
– Determine the speed at which the conveyor chain will be operating. The chain speed is typically expressed in feet per minute or meters per second.
3. Calculate the Chain Pull:
– Determine the total weight or force that needs to be moved by the conveyor chain. This includes the weight of the conveyed material and any additional loads or forces acting on the chain.
4. Calculate the Required Tension:
– Use the following formula to calculate the required tension:
Tension = (Chain Pull × Chain Speed) / (Chain Pitch × Efficiency)
– The efficiency factor accounts for losses due to friction and other factors and is typically expressed as a decimal between 0 and 1.
5. Determine the Maximum Allowable Tension:
– The maximum allowable tension is determined by the manufacturer’s specifications for the conveyor chain. It is important to consult the manufacturer’s documentation or contact them directly to obtain the maximum allowable tension value.
6. Compare the Required Tension and Maximum Allowable Tension:
– Compare the calculated required tension with the maximum allowable tension. The required tension should be less than or equal to the maximum allowable tension to ensure safe and reliable operation of the conveyor chain.
By following these steps and considering the manufacturer’s specifications, you can accurately calculate the maximum allowable tension in a conveyor chain and ensure that it is within the safe operating limits.
What are the advantages of using a plastic conveyor chain?
Plastic conveyor chains offer several advantages over traditional metal chains. Here are some of the key advantages:
1. Corrosion Resistance: Plastic chains are highly resistant to corrosion, making them ideal for applications in humid or corrosive environments. They do not rust or deteriorate when exposed to moisture or chemicals.
2. Lightweight: Plastic chains are significantly lighter than metal chains, making them easier to handle and install. Their lightweight nature reduces the overall weight of the conveyor system and can result in energy savings during operation.
3. Low Noise Operation: Plastic chains generate less noise compared to metal chains, leading to a quieter working environment. This can be particularly beneficial in industries where noise reduction is important, such as food processing or packaging.
4. Reduced Friction and Wear: Plastic chains have self-lubricating properties, which reduce friction and wear. This results in lower maintenance requirements and longer chain life. The smooth surface of plastic chains also minimizes the risk of product damage during transportation.
5. Flexibility and Modularity: Plastic chains can be easily customized and designed to fit specific conveyor system requirements. They offer flexibility in terms of length, width, and configuration. Additionally, plastic chains are often modular, allowing for easy replacement of damaged or worn-out sections without replacing the entire chain.
6. Cost-Effective: Plastic conveyor chains are generally more cost-effective compared to metal chains. They are often less expensive to manufacture and offer a longer lifespan with minimal maintenance requirements, resulting in lower overall costs.
7. Chemical Resistance: Plastic chains are resistant to a wide range of chemicals, making them suitable for applications where exposure to aggressive substances is a concern. They can withstand contact with oils, acids, alkalis, and various cleaning agents.
Overall, the advantages of using a plastic conveyor chain include corrosion resistance, lightweight design, low noise operation, reduced friction and wear, flexibility, cost-effectiveness, and chemical resistance. These benefits make plastic chains a popular choice in various industries, including food processing, packaging, pharmaceuticals, and logistics.
What are the maintenance requirements for a conveyor chain?
Maintaining a conveyor chain is essential to ensure its smooth operation and prolong its lifespan. Here are some key maintenance requirements for a conveyor chain:
- Regular Cleaning: Clean the conveyor chain regularly to remove dirt, debris, and contaminants that can contribute to chain wear and reduce performance. Use appropriate cleaning agents and tools to avoid damaging the chain.
- Lubrication: Apply the recommended lubricant to the conveyor chain according to the manufacturer’s guidelines. Lubrication helps reduce friction, minimize wear, and prevent corrosion.
- Tension Adjustment: Check the tension of the conveyor chain regularly and adjust it if necessary. Proper tension ensures smooth operation and prevents issues like chain slipping or excessive wear.
- Inspection: Conduct regular inspections of the conveyor chain to identify any signs of wear, damage, or misalignment. Look for issues such as worn sprockets, elongation, bent or damaged links, and loose connections. Address any problems promptly to prevent further damage.
- Replace Worn Components: If any components of the conveyor chain, such as links, pins, or sprockets, are excessively worn or damaged, they should be replaced. Using worn components can compromise the chain’s performance and lead to failure.
- Alignment: Ensure proper alignment of the conveyor chain by checking the alignment of sprockets, idlers, and other components. Misalignment can cause uneven wear and increase the risk of chain failure.
- Training and Education: Provide proper training to personnel responsible for operating and maintaining the conveyor chain. They should understand the maintenance requirements, safety protocols, and best practices to ensure effective and safe operation.
Following these maintenance requirements will help keep the conveyor chain in optimal condition, minimize downtime, and ensure safe and efficient material handling.
editor by CX 2024-01-11